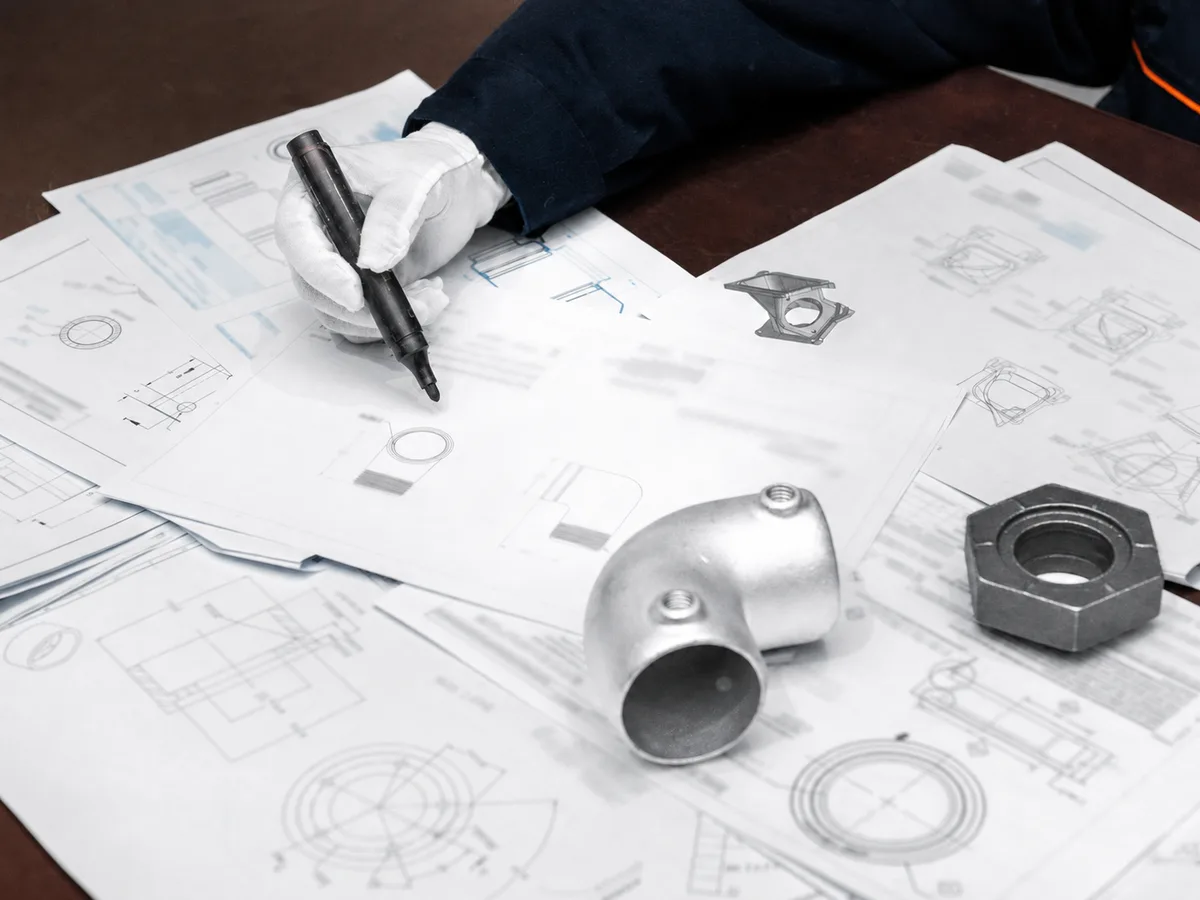
Struggling to make sense of wildly different supplier quotes? When you source custom metal parts, unpredictable investment casting pricing can quickly ruin your project budget. The solution starts with understanding that cost is never based on material weight alone.
Investment casting pricing is determined by the complete manufacturing path required to deliver a finished part. This includes material grade, part geometry, tooling complexity, expected production yield, secondary machining operations, surface finishing, quality inspection requirements, and total order volume. Accurate pricing requires a fully defined project scope.
How do all these variables interact on your final invoice? Let us break down the real drivers behind these costs so you can evaluate supplier quotes with confidence and avoid hidden production expenses.
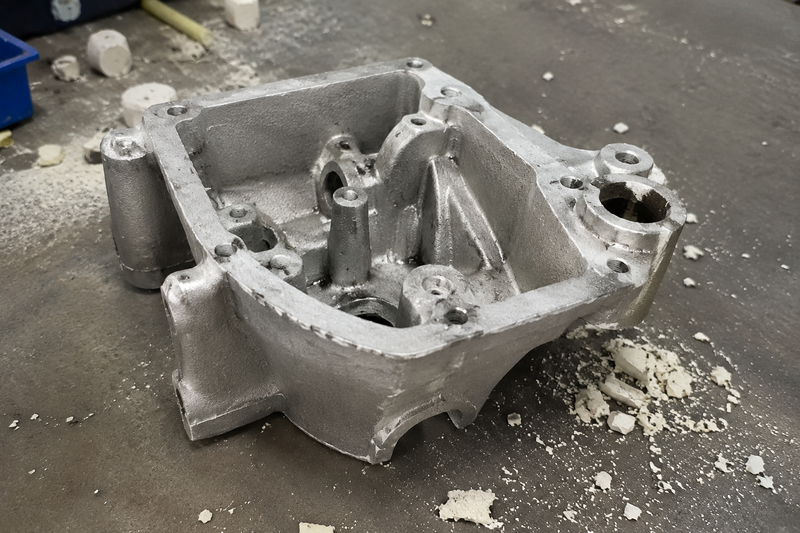
Why Does Part Geometry Affect Investment Casting Pricing?
You might think a small part should always cost less. But complex designs often cause casting defects, leading to frustrating delays. Understanding how geometry affects manufacturability helps you control costs early.
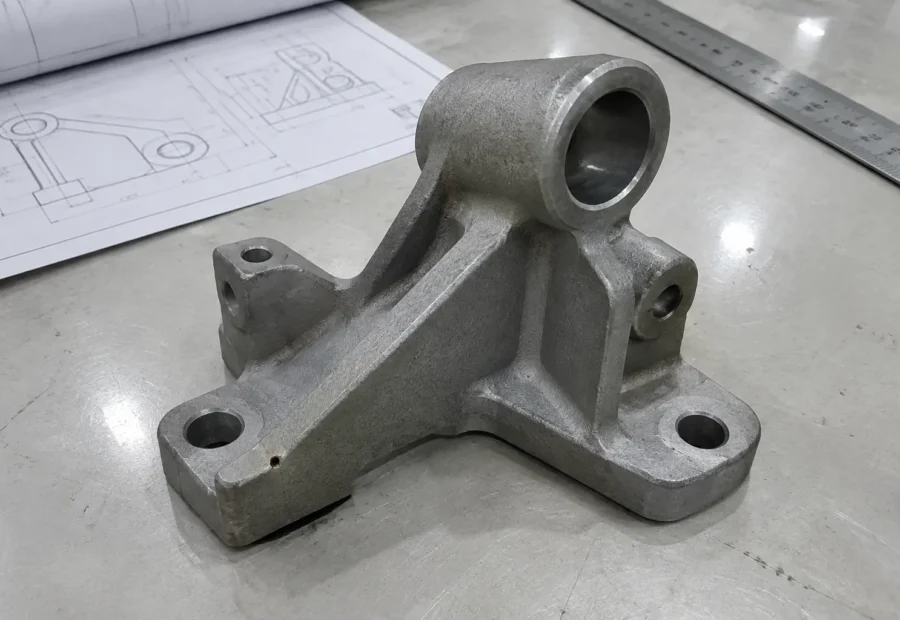
Part geometry directly impacts investment casting pricing by determining tooling complexity, gating system design, and production yield. Highly intricate shapes with demanding tolerances increase process risk. These designs often require specialized wax injection setups, longer cooling times, or higher scrap rates, which ultimately raise the unit cost.
In our quoting experience, geometric complexity is the largest hidden cost driver. A heavy, simple block is often cheaper to cast than a lightweight, thin-walled housing with intricate internal cavities.
The Role of Process Risk and Yield
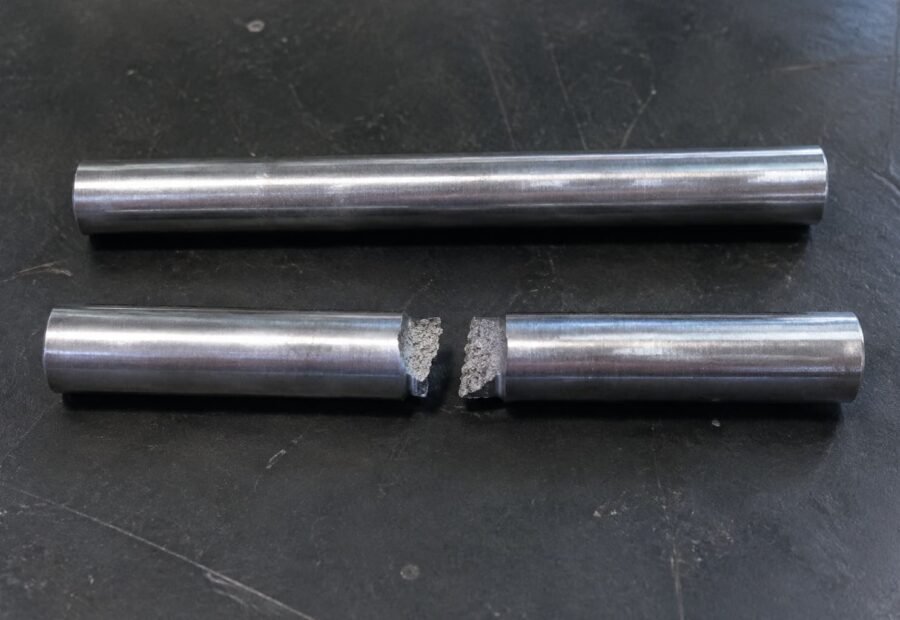
When we review a new 3D model, we immediately look for process risk. Will the molten metal flow evenly throughout the ceramic shell? Will the part warp as it cools? If a design features uneven wall thicknesses or sharp internal corners, the risk of shrinkage, porosity, or cracking goes up significantly.[1]
To compensate for these risks, foundries must modify the gating system (the channels that feed metal into the mold)[2] or accept a lower yield rate. Yield rate is the percentage of acceptable parts per production batch. A lower yield means a higher cost per successful part. We must price the part to account for the metal and labor wasted on the scrapped units.
Design for Manufacturability (DFM)
I always ask our clients a critical question during the quotation phase: "Are all these tight tolerances functionally necessary?"Sometimes, product development engineers apply a blanket high-precision tolerance across the entire technical drawing. This forces us to increase inspection time and scrap perfectly functional parts just because a non-critical dimension is slightly off.
Here is how different geometric features impact your final quotation:
| Feature | Manufacturing Impact | Cost Effect |
|---|---|---|
| Thin Walls (< 3mm) | Harder to fill, requires hotter metal and faster pouring[3] | Increases scrap rate and unit cost |
| Internal Cavities | Requires complex soluble wax or pre-formed ceramic cores[4] | High initial tooling and labor cost |
| Blanket Tolerances | Forces unnecessary CNC machining or high rejection rates | Drastically increases total cost |
| Uniform Walls | Promotes smooth metal flow and predictable cooling | Lowers defect rates and unit cost |
By working closely with you on DFM before finalizing the quote, we can often simplify features, improve production yield, and stabilize your mass production pricing.
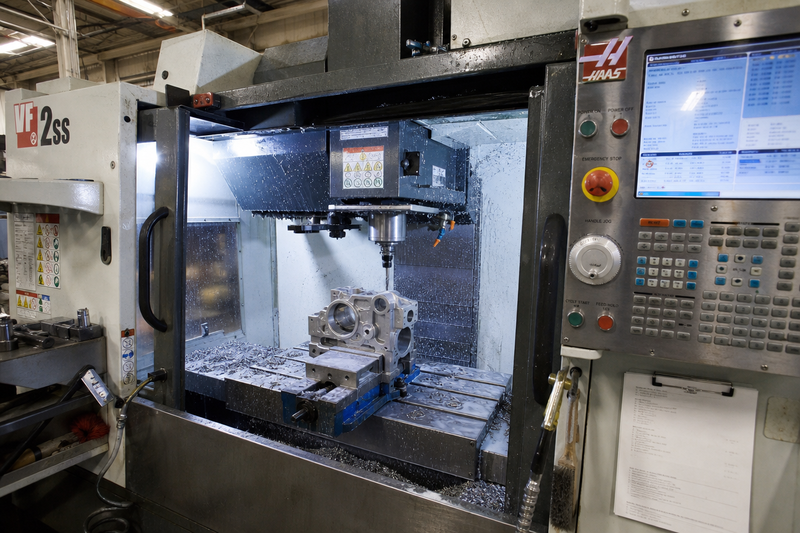
How Do Secondary Operations Impact Investment Casting Pricing?
Many buyers celebrate finding a remarkably low casting quote. However, they soon realize the raw casting cannot be used straight out of the box. Secondary operations often make up the bulk of your final cost.
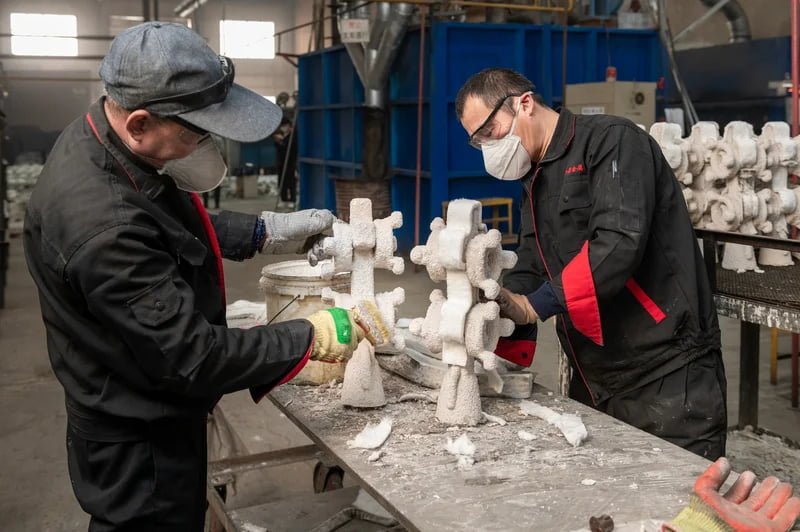
Secondary operations like CNC machining, heat treatment, and surface finishing significantly impact investment casting pricing. The cost of a raw cast part is only a fraction of the finished component. Every drilled hole, milled surface, polished finish, and anodized layer adds labor, machine time, and specialized tooling costs.
As a long-term manufacturing partner, I see this misunderstanding frequently. A client sends a raw casting drawing to one supplier and a fully finished component drawing to us. They then wonder why our quote is higher. We are quoting a completely different scope of work.
The Gap Between Cast Cost and Finished Cost
Investment casting produces an excellent "near-net shape," but functional tolerances almost always require secondary precision work.[5] Threaded holes, precise mating surfaces, and O-ring grooves cannot simply be cast to final dimensions.
When evaluating supplier quotes, you must check what specific operations are included. A complete manufacturing path usually involves several steps:
- CNC Machining: Milling, turning, drilling, and tapping are required to hit critical geometric tolerances that casting alone cannot achieve.
- Heat Treatment: Processes like annealing, normalizing, or hardening are necessary to meet the mechanical strength requirements of your chosen alloy.[6]
- Surface Preparation: Sandblasting or shot peening is required to remove casting scale and smooth the surface.
- Surface Finishing: Polishing, electroplating, painting, powder coating, or anodizing protect the metal against corrosion and improve aesthetics.
I once reviewed a pump housing project where the raw casting accounted for only 30% of the total unit price. The remaining 70% came from a complex 5-axis CNC machining operation and a highly specialized anti-corrosion coating. If you only compare the raw casting price per kilogram, you are missing the bigger picture. Defining the exact finishing operations, packaging, and inspection requirements upfront ensures accurate and comparable quotes.
Does Order Volume Reduce Investment Casting Pricing?
You might assume that doubling your order size will cut your unit price in half. When the discount is tiny, buyers feel cheated. The reality of manufacturing scale is much more complex.
Order volume does reduce investment casting pricing, but only up to a certain point. Higher volumes allow suppliers to spread fixed costs across more parts. However, recurring costs like raw materials, energy, and manual labor remain constant per part regardless of the batch size.
It is a common misconception that high volume guarantees massive cost reductions. Let us look at how scale actually works in a custom OEM manufacturing environment.
Fixed Costs vs. Recurring Costs
Your initial investment casting tooling (the aluminum mold used to inject the wax patterns) is a fixed cost. If a mold costs $3,000, that tooling adds $3.00 per part for a 1,000-piece order. If you order 10,000 pieces, the tooling cost drops to $0.30 per part.
Similarly, the time spent setting up CNC machines for secondary operations is fixed per batch. Running larger batches dilutes this setup cost. We only have to program the machine, load the custom fixtures, and calibrate the tools once for a run of 2,000 parts, compared to doing it four times for four separate runs of 500 parts.
The Limits of Economies of Scale
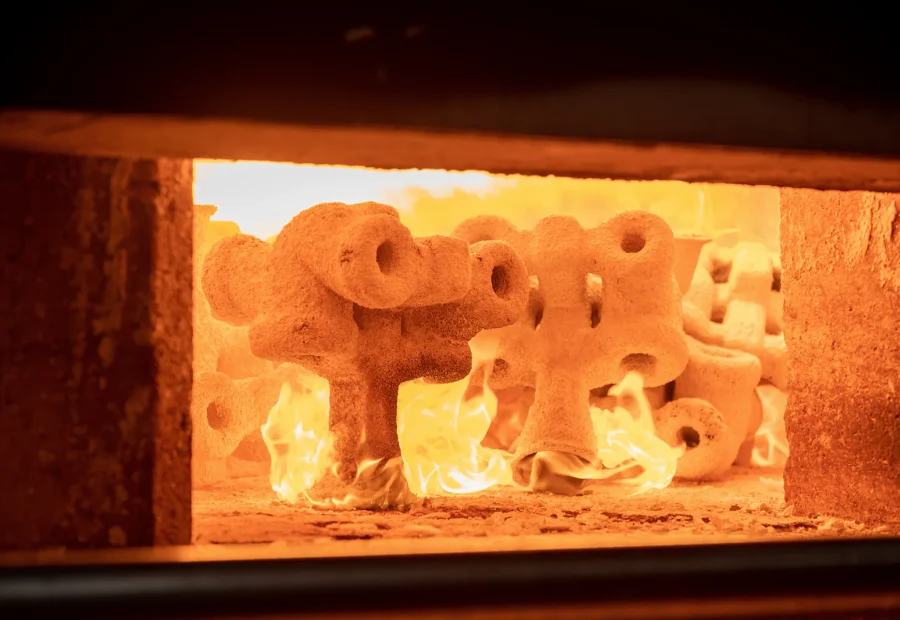
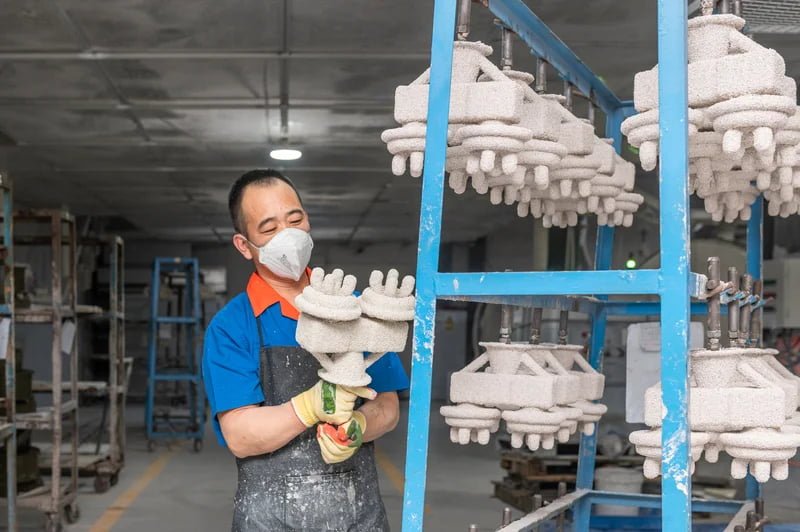
However, investment casting remains a fundamentally labor-intensive and energy-intensive process. Wax trees must be assembled by hand. Ceramic shells must dry in climate-controlled rooms for days.[7] Induction furnaces consume massive amounts of electricity to melt steel or aluminum.[8]
- Raw Materials: Metal alloys trade on global commodity markets. Volume discounts on raw stainless steel or aluminum are minimal, even for large factories.
- Labor: Grinding off gates, inspecting parts visually, and packing boxes take the exact same amount of time per unit whether you order 500 pieces or 5,000 pieces.
- Annual vs. Batch Volume: Procurement managers often quote an "annual volume" of 12,000 parts but demand delivery in batches of 1,000 every month. This schedule does not yield a 12,000-piece discount. We still have to set up our machines and manage production 12 separate times.
In our quoting experience, once you pass a certain batch threshold, the unit price plateaus. The recurring material, energy, and labor costs establish a hard floor for your investment casting pricing.
What Hidden Risks Change Investment Casting Pricing?
Comparing two quotes based purely on the bottom-line number is dangerous. If one supplier omits vital quality checks, your cheap parts will eventually cause an expensive assembly line failure.
Hidden risks change investment casting pricing when suppliers have different assumptions about the project scope. Differences in inspection protocols, material certifications, non-destructive testing, and defect liability drastically alter the real cost. A quote that ignores mass production stability will ultimately cost you more in delays.
The lowest initial unit price may simply transfer the costs of rework, delayed shipments, and supplier switching back to your company. We have helped many clients who initially chose a cheaper supplier, only to face severe delivery and quality issues during mass production.
The "Sample Trap"
Producing five perfect samples in a controlled laboratory environment is relatively easy. Producing 5,000 identical parts over six months is incredibly hard. Some suppliers quote aggressively low prices just to win your tooling order. They manually tweak and carefully machine the initial samples to pass your First Article Inspection (FAI).
But when mass production starts, their unstable baseline process results in high scrap rates. They quickly realize they are losing money. This leads them to demand a sudden price increase, compromise on material quality, or constantly delay your shipments. A credible quote must support stable, repeatable mass production from day one.
Quality Control and Traceability
Quality documentation is a major pricing variable that often goes unnoticed. If your part goes into industrial equipment, fluid valves, or automotive systems, you need verifiable proof of quality.
Key quality drivers include:
- Material substitution rules: Did the supplier quote the exact alloy you requested, or did they base their price on a cheaper, unverified local equivalent?
- Testing requirements: Do you need X-ray inspection for internal voids? Magnetic particle inspection for surface cracks? Spectrometer analysis for chemical composition?[9] Each test adds time and cost.
- Traceability: Do you require specific heat numbers cast directly into the part and detailed EN 10204 3.1 material test reports (MTRs)[10] delivered with every batch?
When you evaluate investment casting pricing, you are really buying a defined manufacturing path. Always ask suppliers to clarify their assumptions, list their inspection steps, and guarantee their mass-production yield.
Frequently Asked Questions
What is the average tooling cost for investment casting?
Average tooling for investment casting ranges from $1,000 to $5,000 depending on part size, complexity, and whether soluble cores are needed. Unlike die casting molds that withstand immense pressure, investment casting molds only inject low-pressure wax.[11] They cost less to manufacture and last much longer.
Is investment casting cheaper than CNC machining?
Investment casting is generally cheaper than pure CNC machining for complex shapes in medium to high volumes. It drastically reduces material waste and machining time. However, for very low quantities or simple geometric shapes, direct CNC machining from solid billet may be more cost-effective.
Can I get a flat per-kilogram price for investment casting?
We advise against using a flat per-kilogram price. While raw material cost is a factor, two parts weighing 1kg can have vastly different prices based on geometric complexity, tooling requirements, secondary CNC machining, and required surface finishes.
How long does the investment casting quotation process take?
A comprehensive quote usually takes 3 to 5 days. This allows the engineering team to conduct a proper Design for Manufacturability (DFM) review, assess production yield risks, and gather accurate costs for secondary machining and external surface treatments.
Conclusion
Navigating investment casting pricing does not have to be a guessing game. As we have explored, the true cost depends on a fully defined manufacturing path—from part geometry and initial tooling to secondary CNC machining, order volume, and stringent quality inspection. Chasing the lowest bid without comparing the detailed project scope often leads to unstable production, delayed timelines, and hidden rework costs.
We are a dedicated OEM manufacturing partner with over twenty years of experience. We offer one-stop investment casting, die casting, CNC machining, and surface treatment services to ensure your custom metal parts are delivered consistently and cost-effectively. Contact us today with your 3D models and drawings for a comprehensive manufacturability review and an accurate, risk-free quote.
Sources & references
Reference note
Foundry engineering principles demonstrate that abrupt changes in cross-sectional area and sharp internal corners cause localized hot spots and stress concentrations, leading to shrinkage porosity and hot tearing. Evidence role: mechanism; source type: research. Supports: how uneven wall thicknesses and sharp corners lead to differential cooling, shrinkage, and cracking.
Reference note
The gating system is a critical network of channels designed to deliver molten metal into the mold cavity smoothly while providing a reservoir of liquid metal to feed volumetric shrinkage during solidification. Evidence role: definition; source type: education. Supports: the definition and function of gating systems in controlling metal flow and feeding shrinkage.
Reference note
Casting sections thinner than 3mm typically requires increased metal superheat and optimized pouring velocities to ensure complete mold filling before the alloy solidifies. Evidence role: mechanism; source type: paper. Supports: the necessity of higher superheat and faster pouring rates for thin-wall castings. Scope note: Advanced techniques like vacuum-assisted casting can mitigate some of these temperature requirements.
Reference note
To form intricate internal passages that cannot be molded using standard tooling, investment casting relies on pre-formed ceramic cores or soluble wax inserts that are later dissolved or leached out. Evidence role: general_support; source type: research. Supports: the use of ceramic and soluble wax cores to create complex internal geometries in investment casting.
Reference note
While investment casting is classified as a near-net shape process capable of achieving standard linear tolerances (e.g., ISO 8062), critical mating surfaces and tight functional tolerances typically require secondary CNC machining. Evidence role: general_support; source type: institution. Supports: the classification of investment casting as a near-net shape process and its typical tolerance capabilities.
Reference note
Post-casting heat treatments, including annealing, normalizing, and quenching, are routinely employed to homogenize the as-cast microstructure, relieve internal stresses, and achieve the desired balance of hardness and ductility. Evidence role: mechanism; source type: education. Supports: the metallurgical mechanisms by which heat treatments improve the mechanical properties of castings.
Reference note
The shell building phase in investment casting involves applying multiple layers of ceramic slurry and stucco, each requiring strictly controlled temperature and humidity conditions to dry properly, a process that can take several days to complete. Evidence role: general_support; source type: research. Supports: the necessity of controlled temperature and humidity for drying ceramic shells over several days. Scope note: Drying times can be accelerated using advanced polymer-modified binders or specialized drying equipment.
Reference note
Department of Energy reports indicate that melting operations, primarily utilizing induction or electric arc furnaces, account for over half of the total energy consumption in a typical metal casting facility. Evidence role: statistic; source type: government. Supports: the high electrical energy consumption associated with induction melting in foundries. Scope note: Energy efficiency varies significantly based on furnace capacity and operational practices.
Reference note
Standard quality assurance protocols in foundries utilize radiographic testing (X-ray) to detect internal porosity, magnetic particle inspection (MPI) for surface discontinuities, and optical emission spectrometry to verify alloy chemistry. Evidence role: general_support; source type: institution. Supports: the application of radiography for internal voids, MPI for surface defects, and spectrometry for chemical analysis in castings.
Reference note
The EN 10204 3.1 standard specifies a type of inspection document issued by the manufacturer, declaring that the products comply with the order requirements and supplying specific test results validated by an authorized inspection representative. Evidence role: definition; source type: institution. Supports: the definition and requirements of an EN 10204 3.1 material certificate.
Reference note
Investment casting tooling is subjected only to the low pressures required for wax injection, whereas die casting dies must withstand extreme thermal shock and the high injection pressures of molten metal, significantly impacting tooling lifespan and cost. Evidence role: mechanism; source type: education. Supports: the difference in operating pressures between die casting molds and investment casting wax tooling.