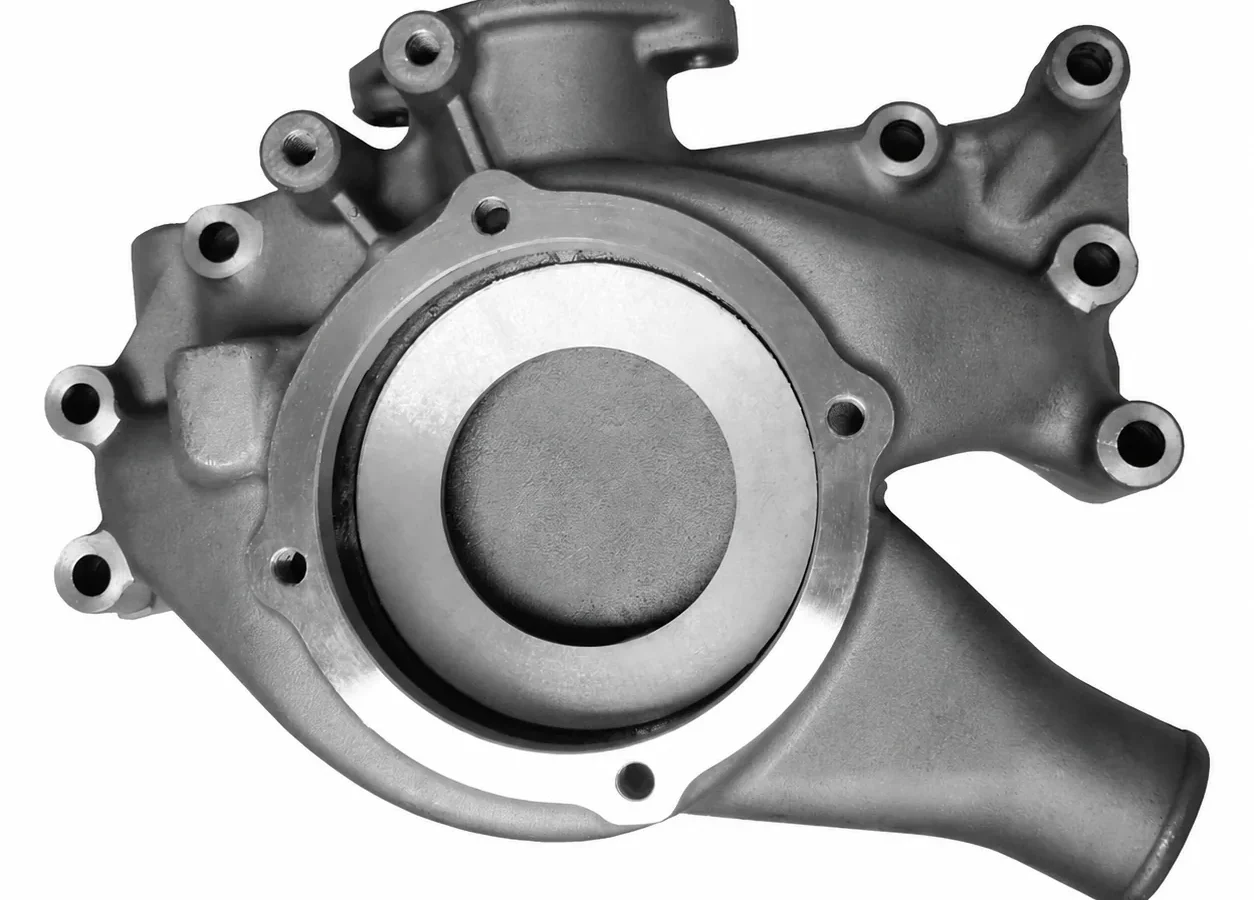
Part and application
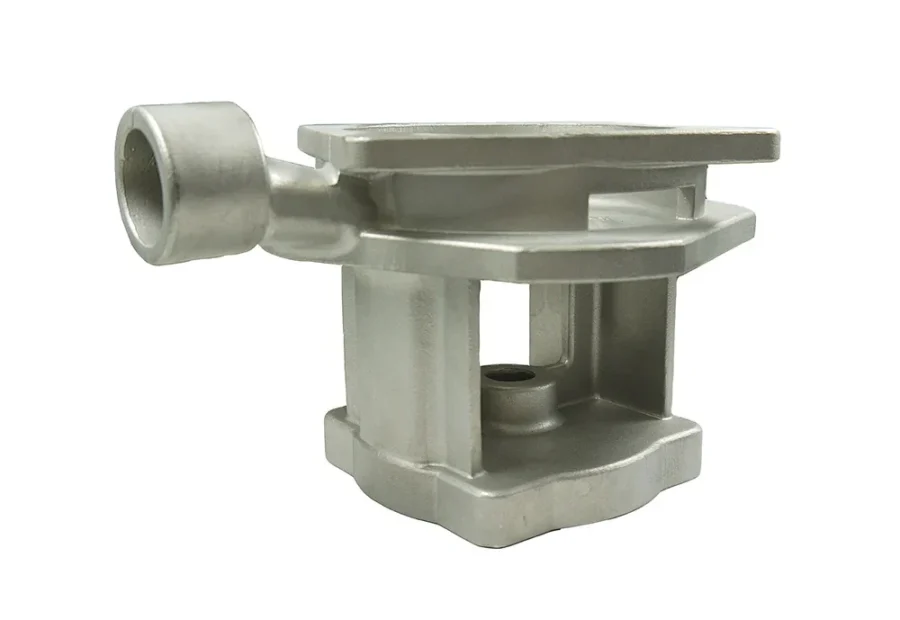
This HT250 gray-iron body is for an engine cooling-water pump in heavy equipment or a high-output diesel engine. It has a large central mounting register, a ring of bolt locations and an internal flow passage. The project used resin-sand molds and cores to form the body and passage before CNC finishing.
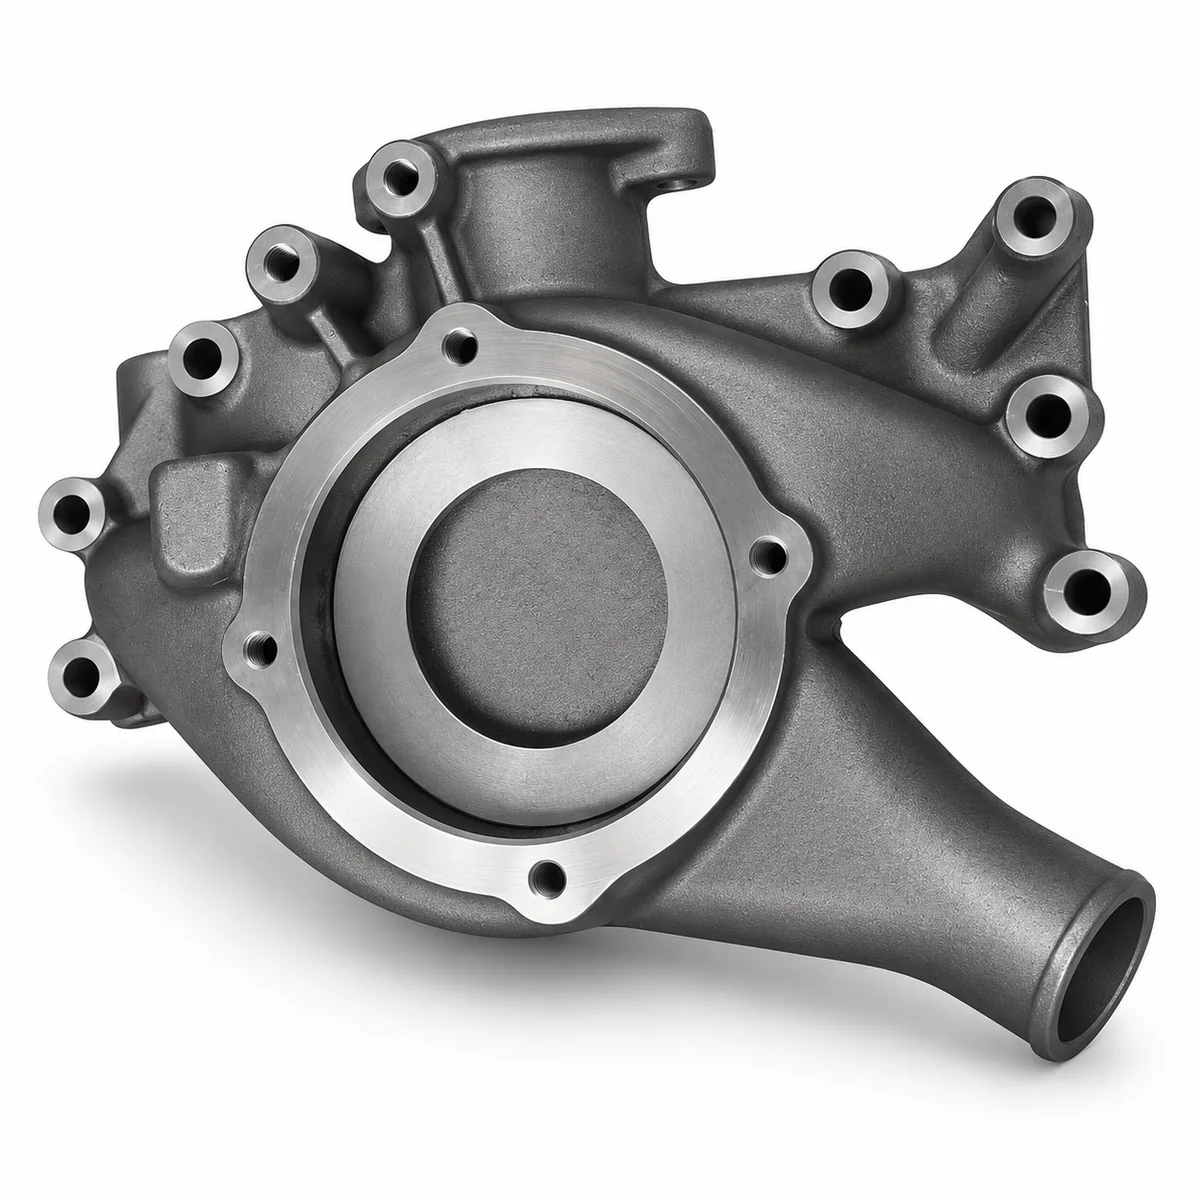
Customer requirements
The customer needed a dense pressure boundary, consistent mounting dimensions and a pump body that would not leak under the specified water test. The central register and flange face were important assembly interfaces. The project specified an IT8 register bore and 0.05 mm flange-face flatness after machining.
Problem encountered
The thick central section was susceptible to shrinkage cavities and dispersed shrinkage porosity as the casting solidified. Defects in that region could affect pressure tightness and leave insufficient sound material near the machined register.
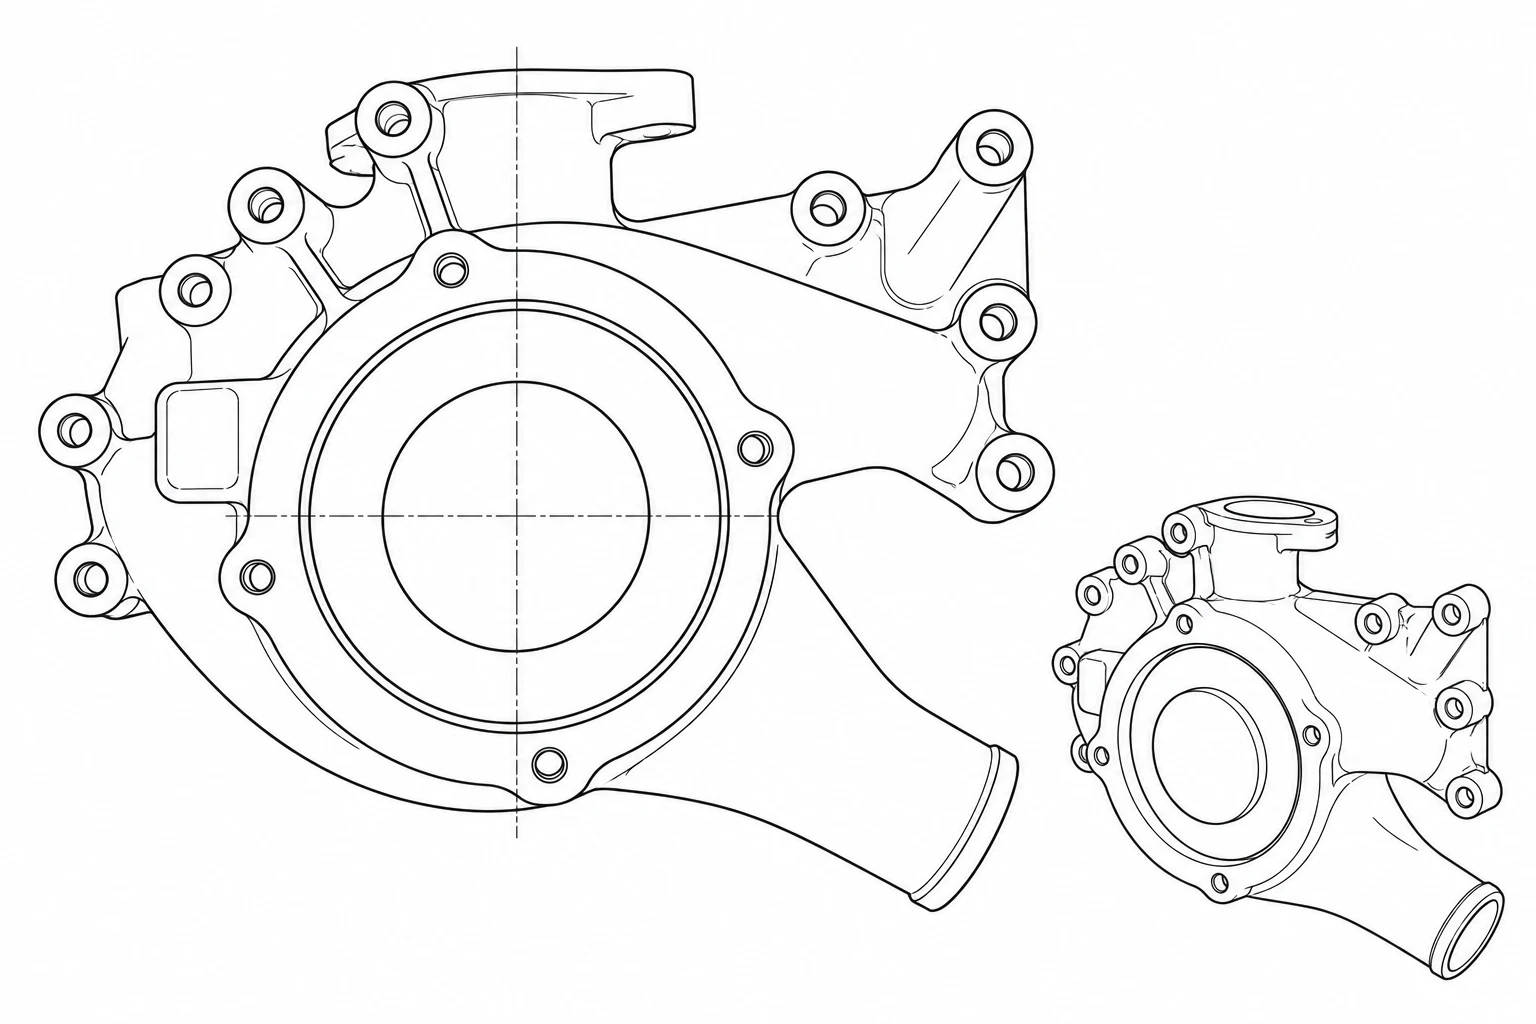
Process changes
The foundry enlarged the riser and adjusted pouring temperature to improve feeding into the central hot spot. Resin-sand mold and core preparation, iron melting, pouring, knockout and cleaning formed the casting route. Natural aging was used before machining to reduce the risk of later movement.
Machining and inspection
CNC machining covered the central register face and bore, flange bolt holes and outlet face. The project inspection route included material test specimens, caliper or CMM dimensional checks, visual inspection and hydrostatic testing. The supplied record reports no leakage at 0.4 MPa after a 5-minute hold.
Reported project result
After the feeding adjustment, the supplied record states that the body met the customer pressure requirement and entered batch delivery.