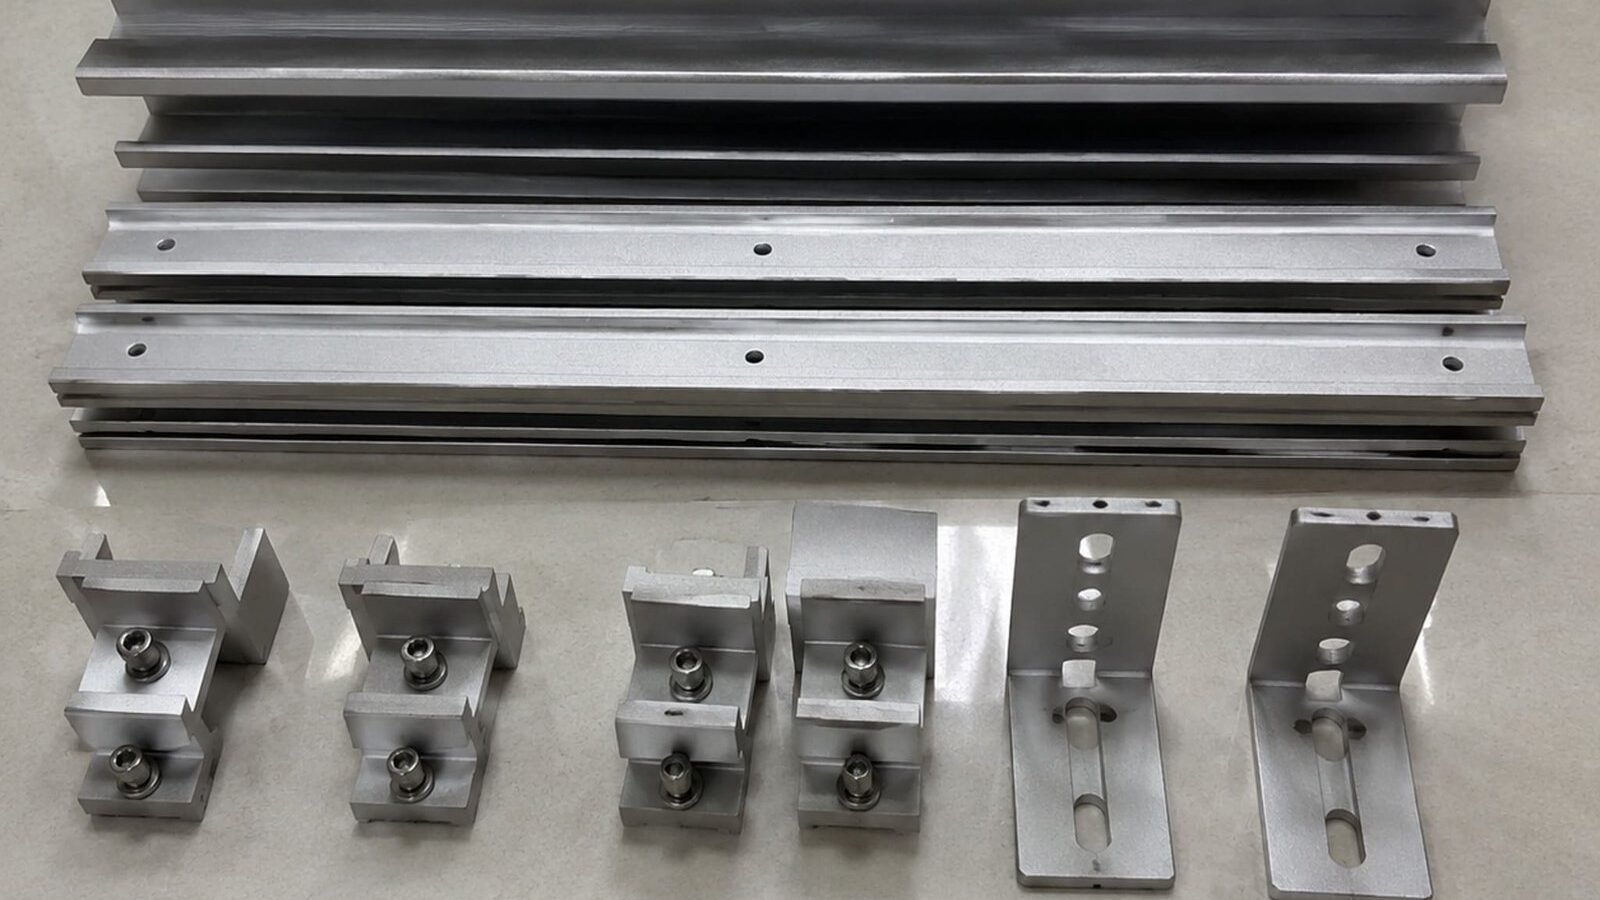
Product: Solar mounting hardware set
Application: Outdoor photovoltaic mounting assemblies
Material: A380 aluminum alloy
Process: High-pressure die casting with trimming and controlled edge finishing
Product and application
The hardware set connects and supports components in outdoor photovoltaic mounting assemblies. Stable interfaces and a controlled edge condition were important because the parts moved through the customer's automated handling and assembly process.
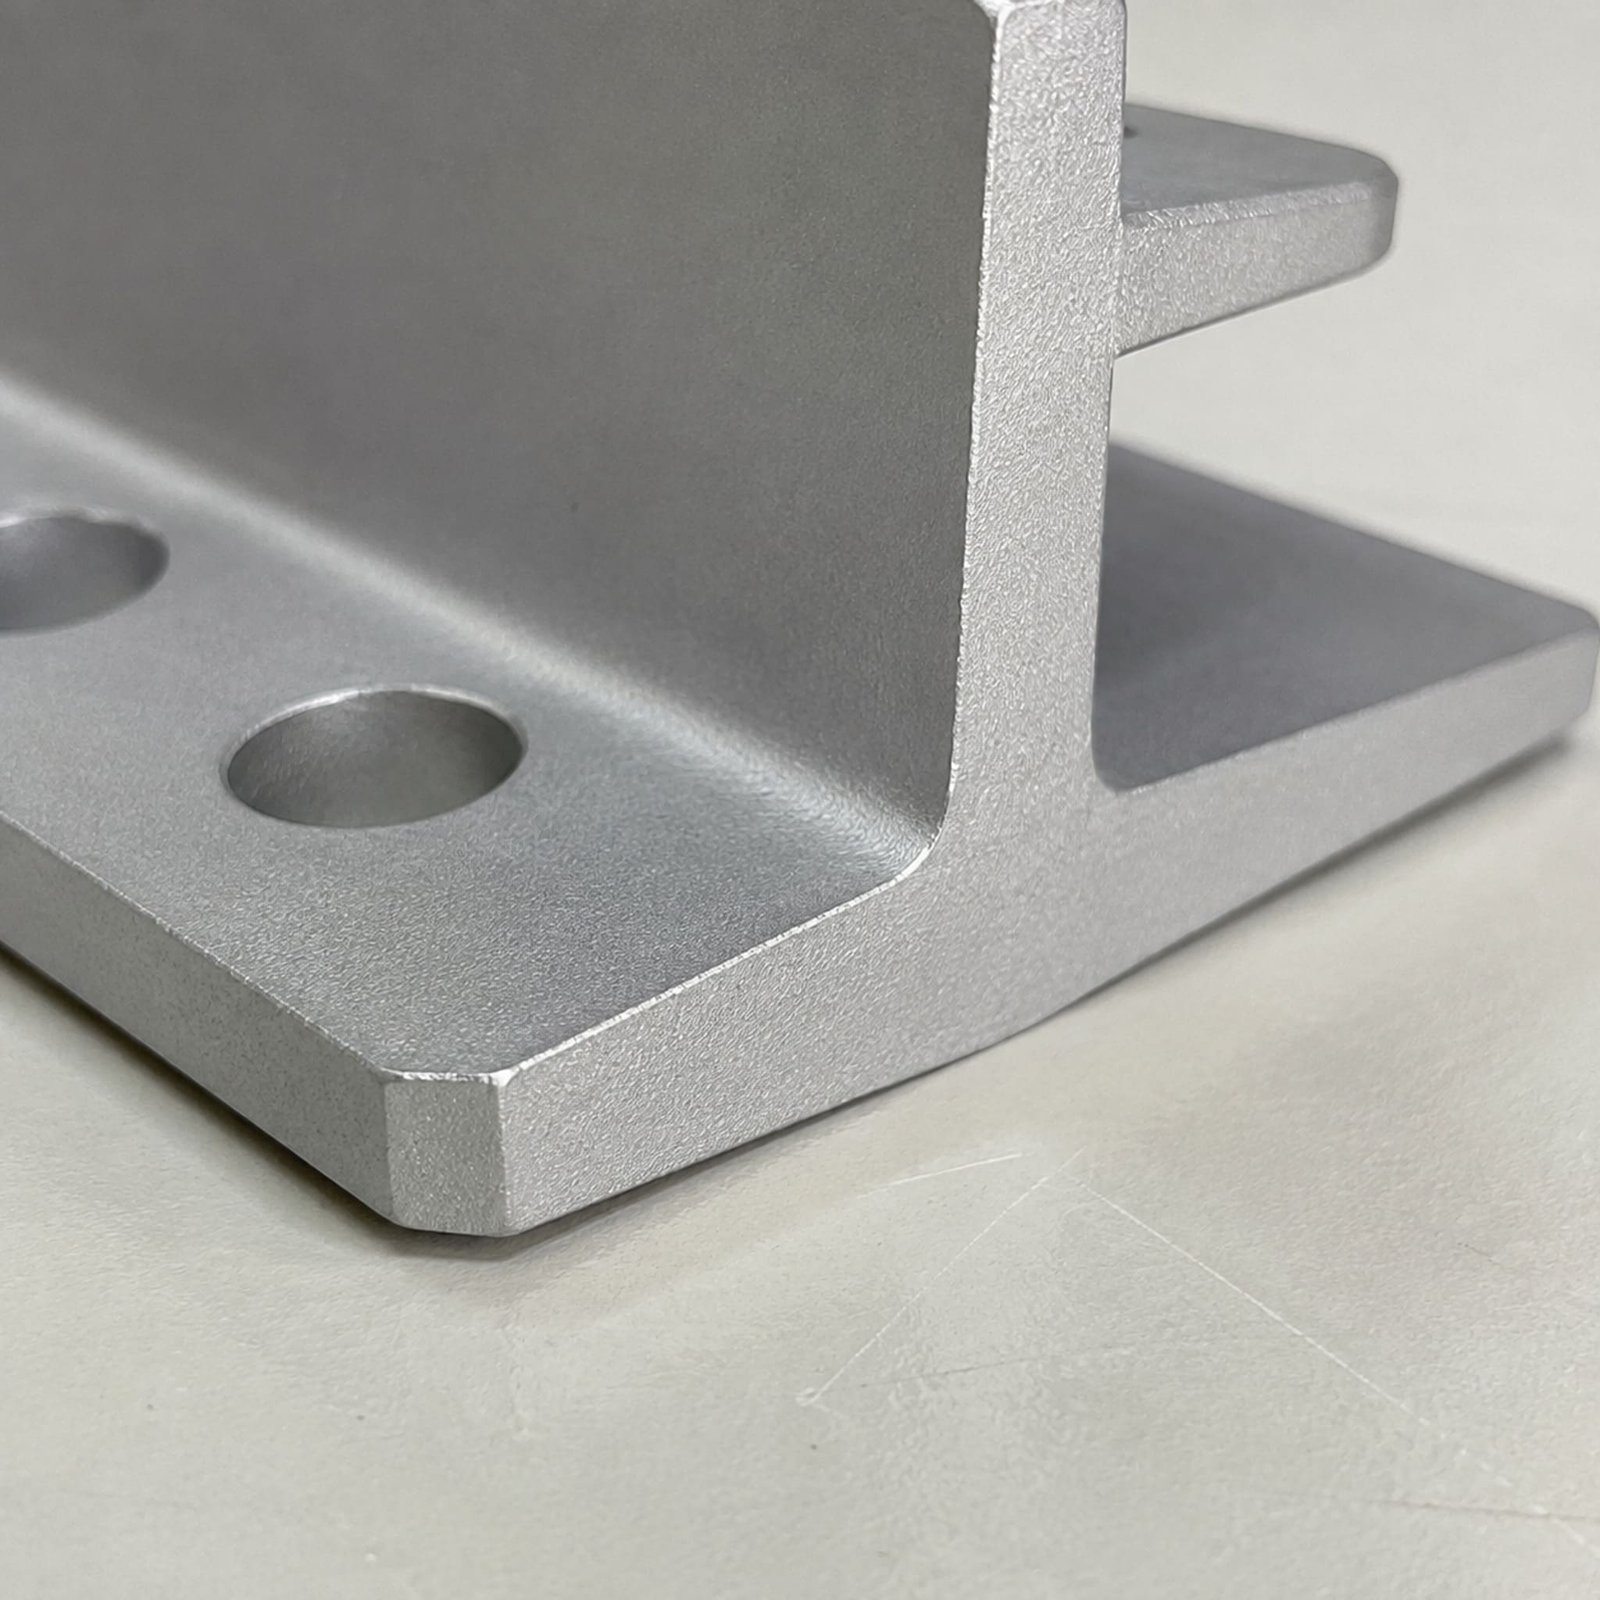
Anonymized bracket detail without customer dimensions or identifiers.
Project challenge
The earlier supply condition included uneven parting-line and edge areas that could interfere with robotic gripping, unpacking and assembly. The revised route therefore had to control both the casting process and the finished edge condition rather than treating appearance as a secondary concern.
Porosity and shrinkage were recorded as project-specific risks. This case does not claim an absolute absence of internal discontinuities because no publishable radiography, CT, sectioning or leakage-test record was supplied.
Manufacturing approach
The route combined tooling review, high-pressure die casting, controlled trimming and standardized finishing of edge, chamfer and parting-line areas. Burrs and sharp edges were removed, and the affected surfaces were leveled for more consistent automated handling.
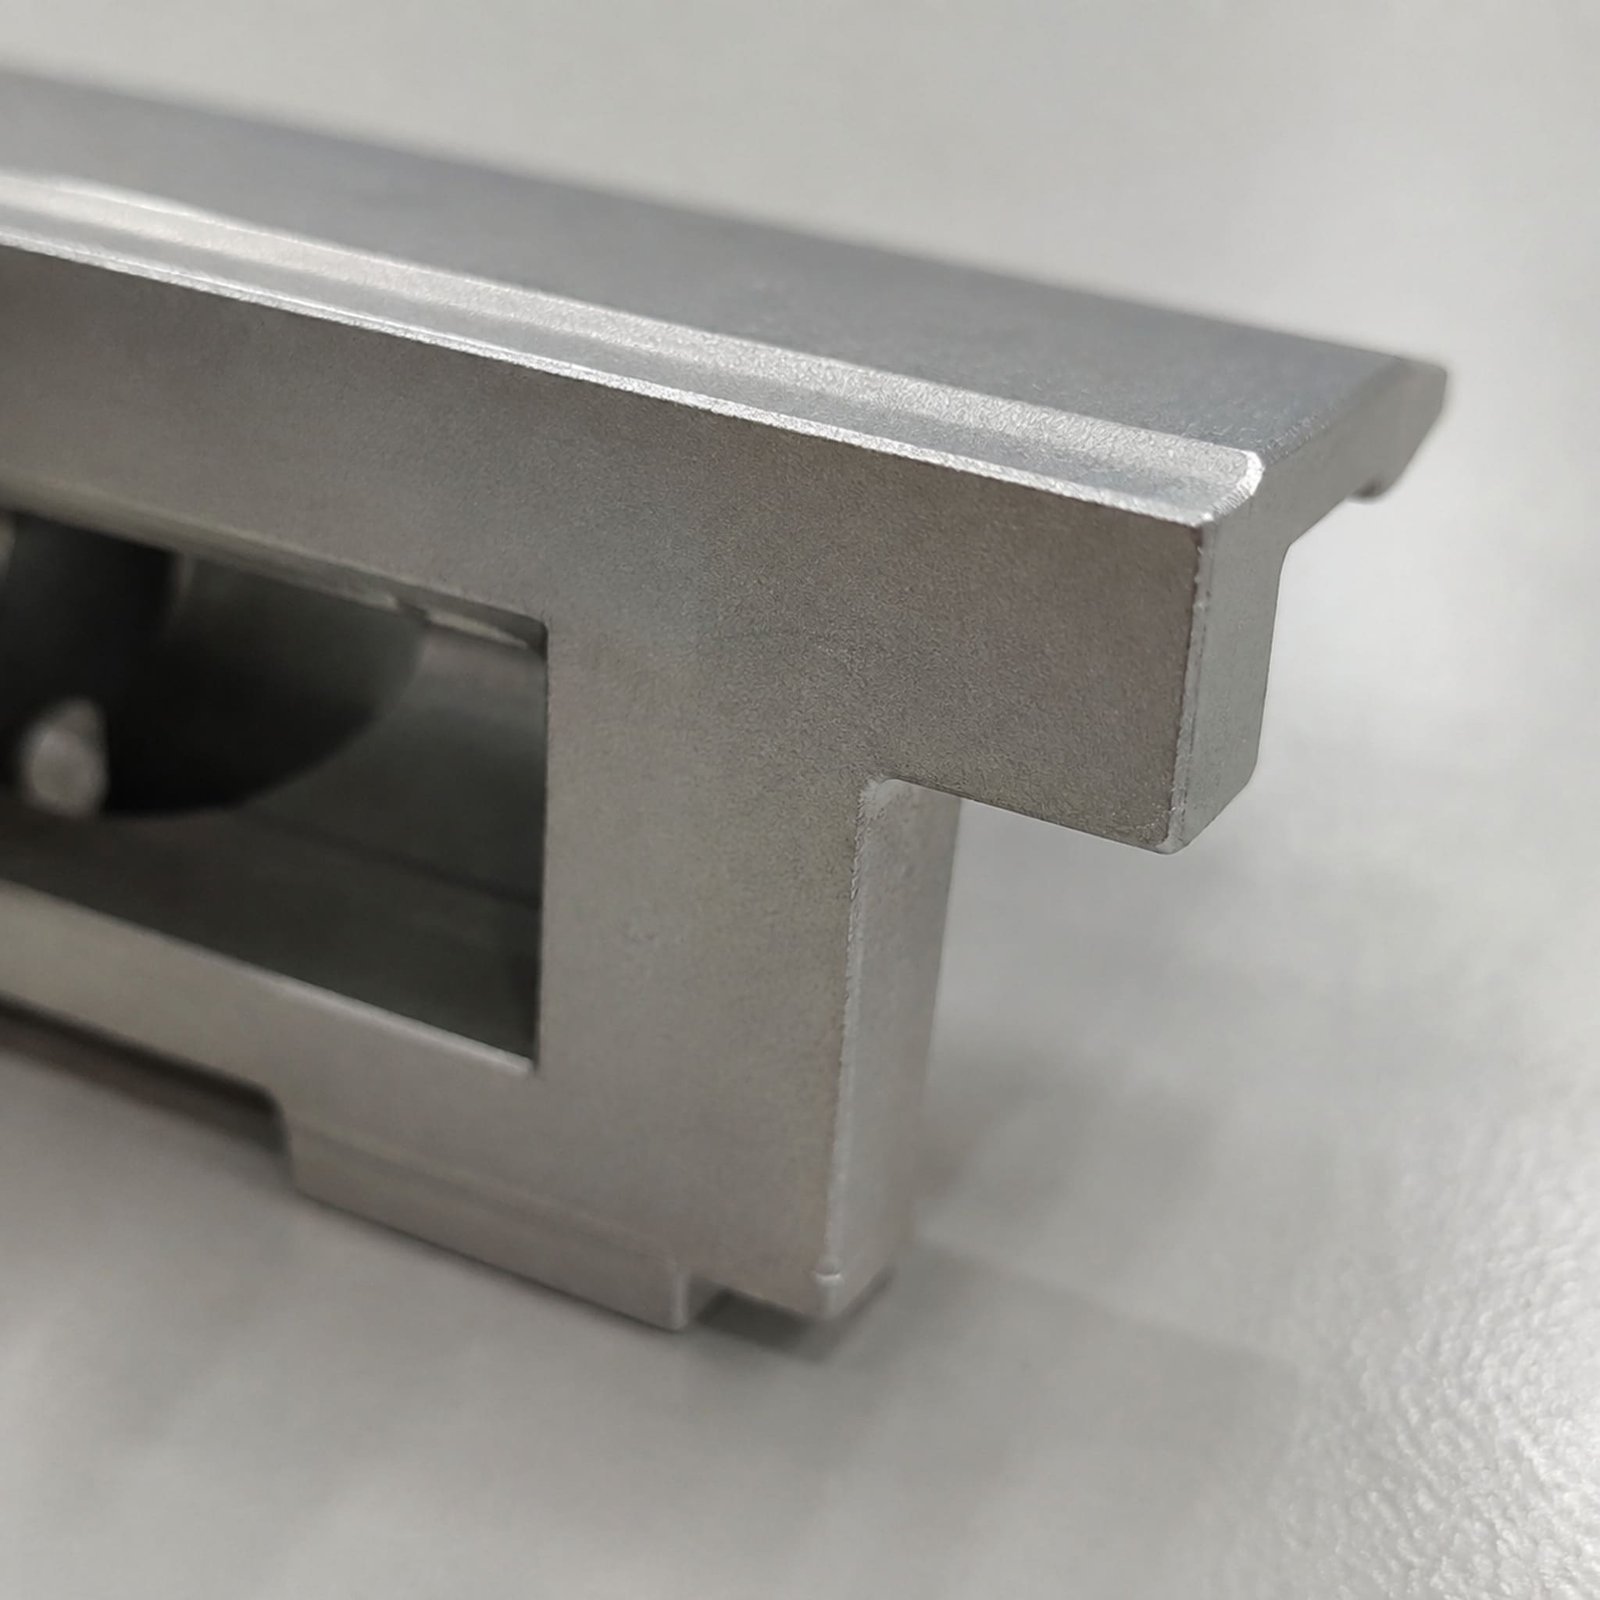
Close view documenting the agreed edge and surface condition.
Verification and outcome
The recorded control plan used first-piece, patrol, final and visual inspection together with 100% inspection of specified finished dimensions. A project-specific ±0.15 mm requirement applied only to identified assembly characteristics.
The project moved from tooling and ten sample sets into repeat production, with approximately 40,000 pieces planned per year in quarterly batches. Customer identity, prices, controlled drawings and unapproved performance percentages remain undisclosed.