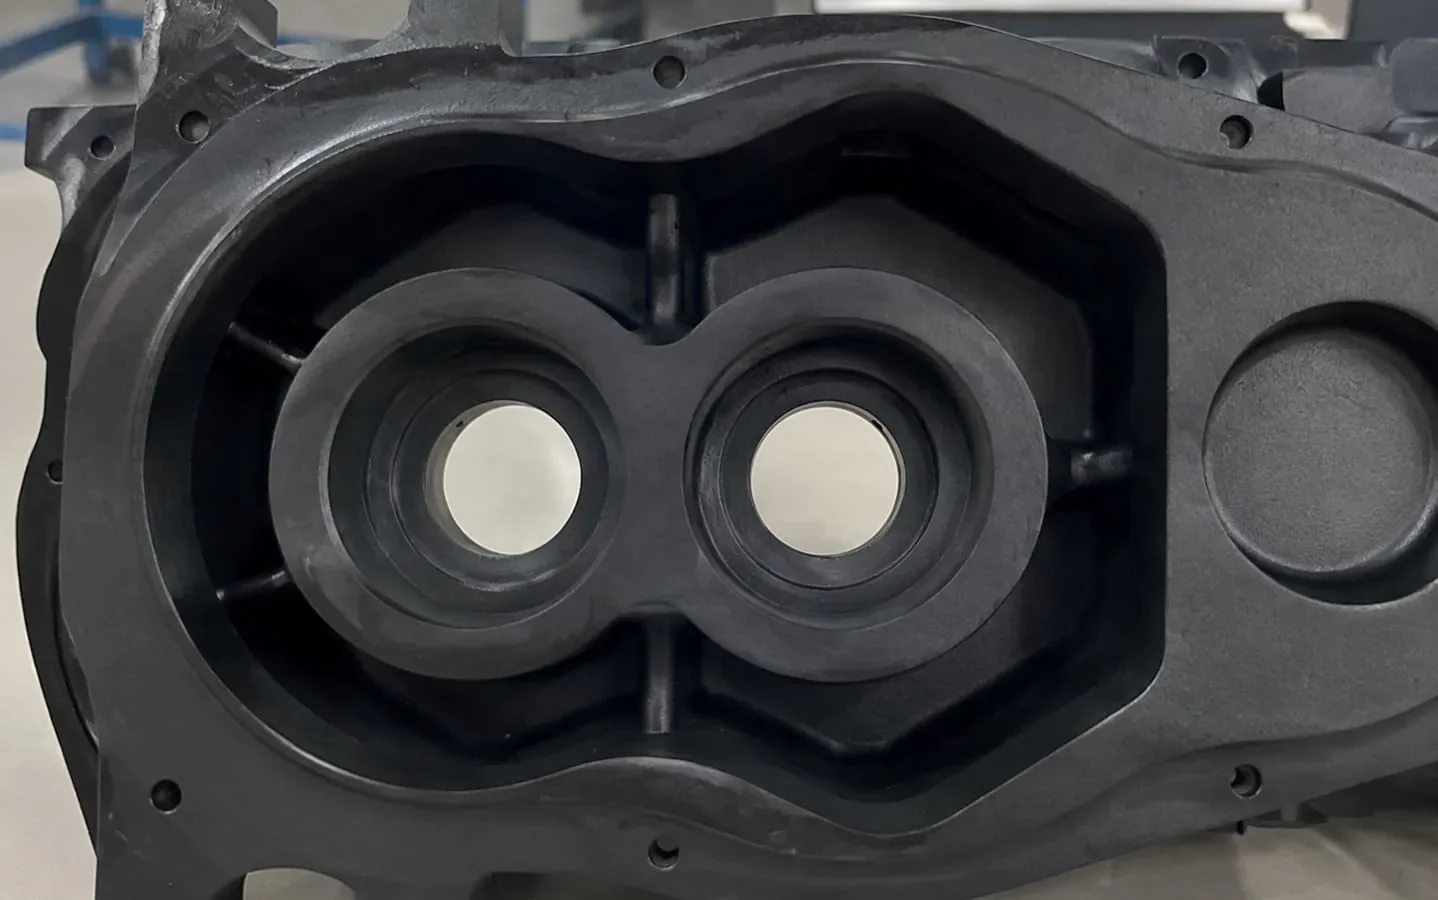
Product: Die-cast equipment housing
Application: Construction and industrial equipment
Material: A356 aluminum alloy in the revised project route
Process: Die casting with machining, coating and project-specific inspection
Product and application
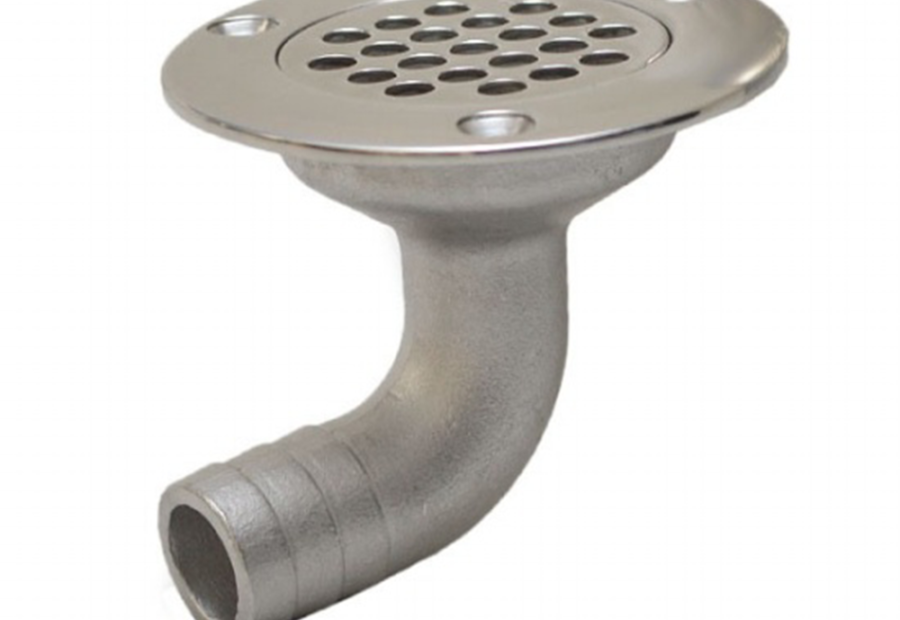
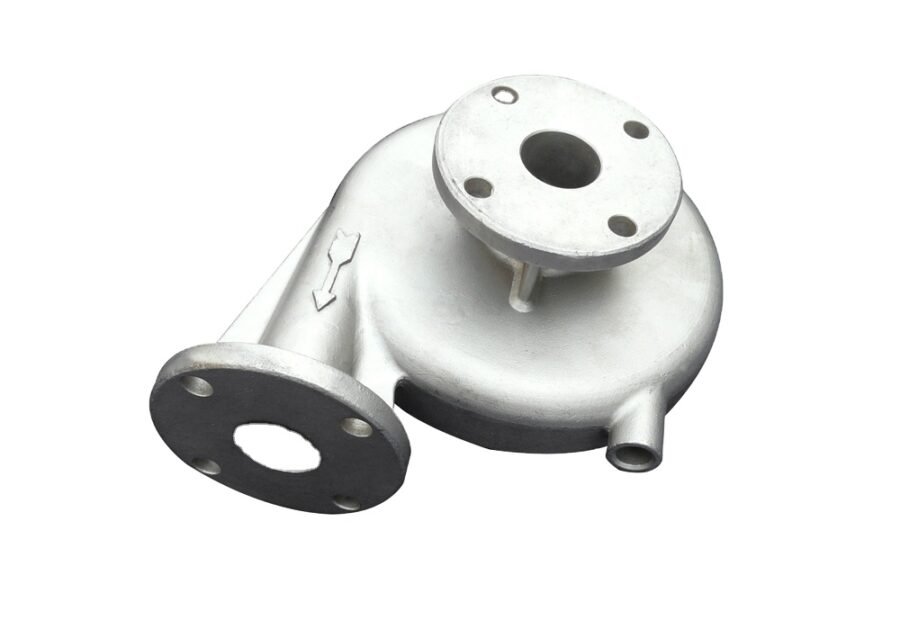
The housing is used in equipment where machined interfaces, assembly fit and leakage-sensitive service conditions must be controlled. The customer also required a finished condition compatible with automated unpacking and assembly.
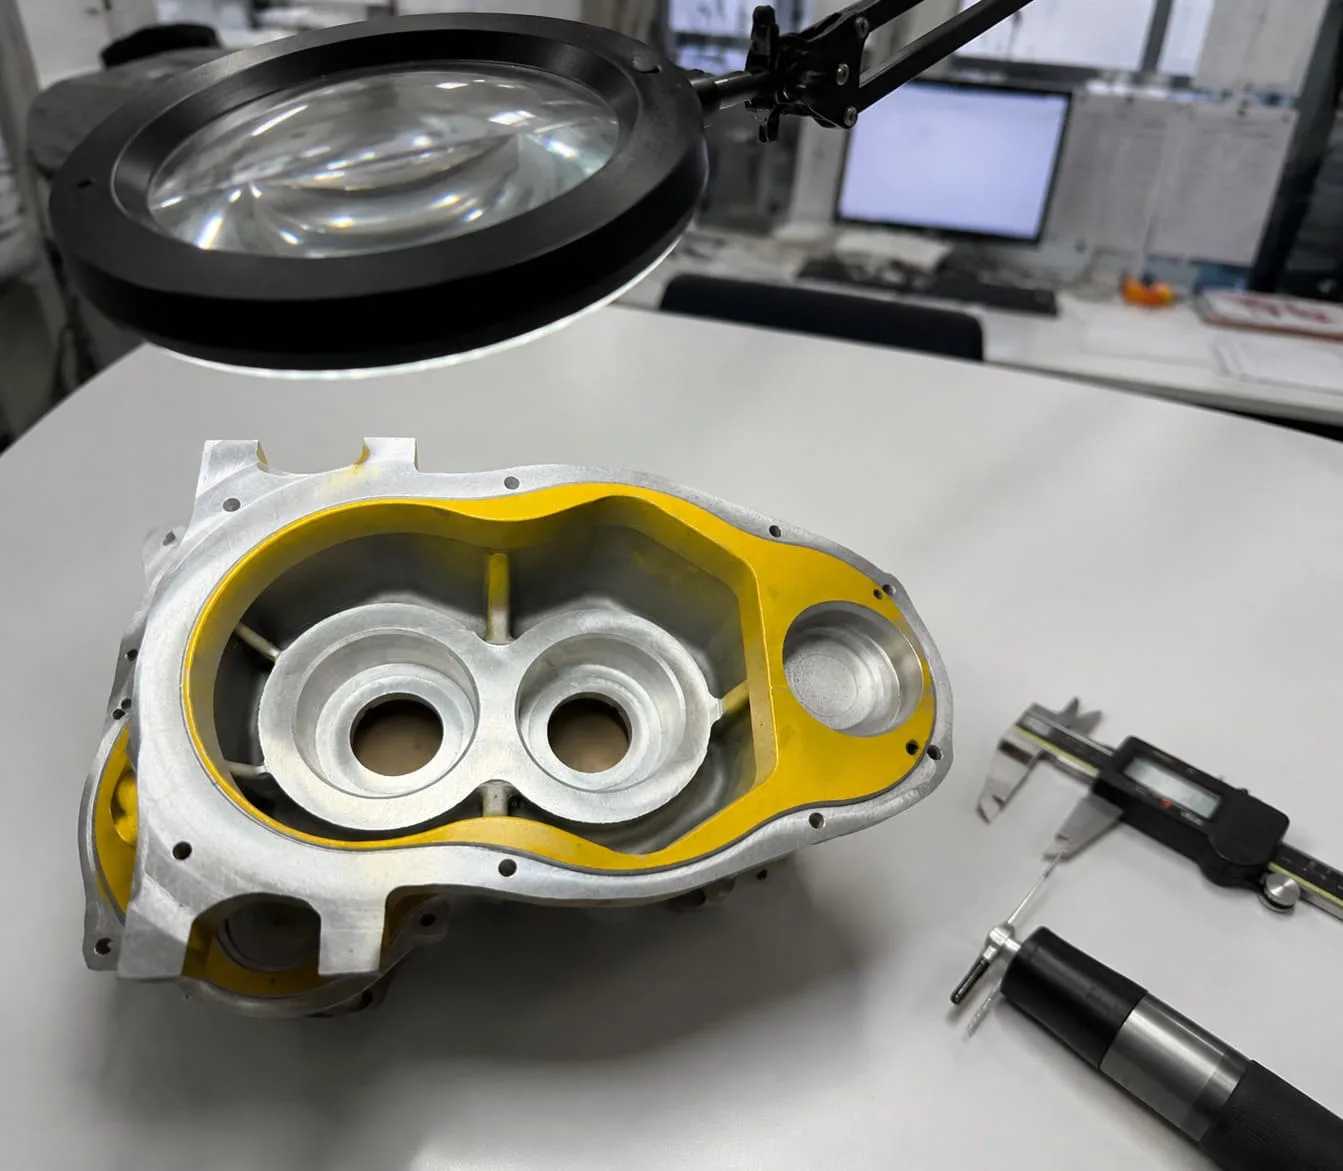
Dimensional review of the housing without publishing controlled values.
Project challenge
The first samples did not reveal the later production issue. During assembly of the first small batch, the customer reported leakage after five machines had been assembled. The supplied evidence indicated internal porosity that became visible only after coating and machining, showing that appearance checks alone were insufficient for the affected area.
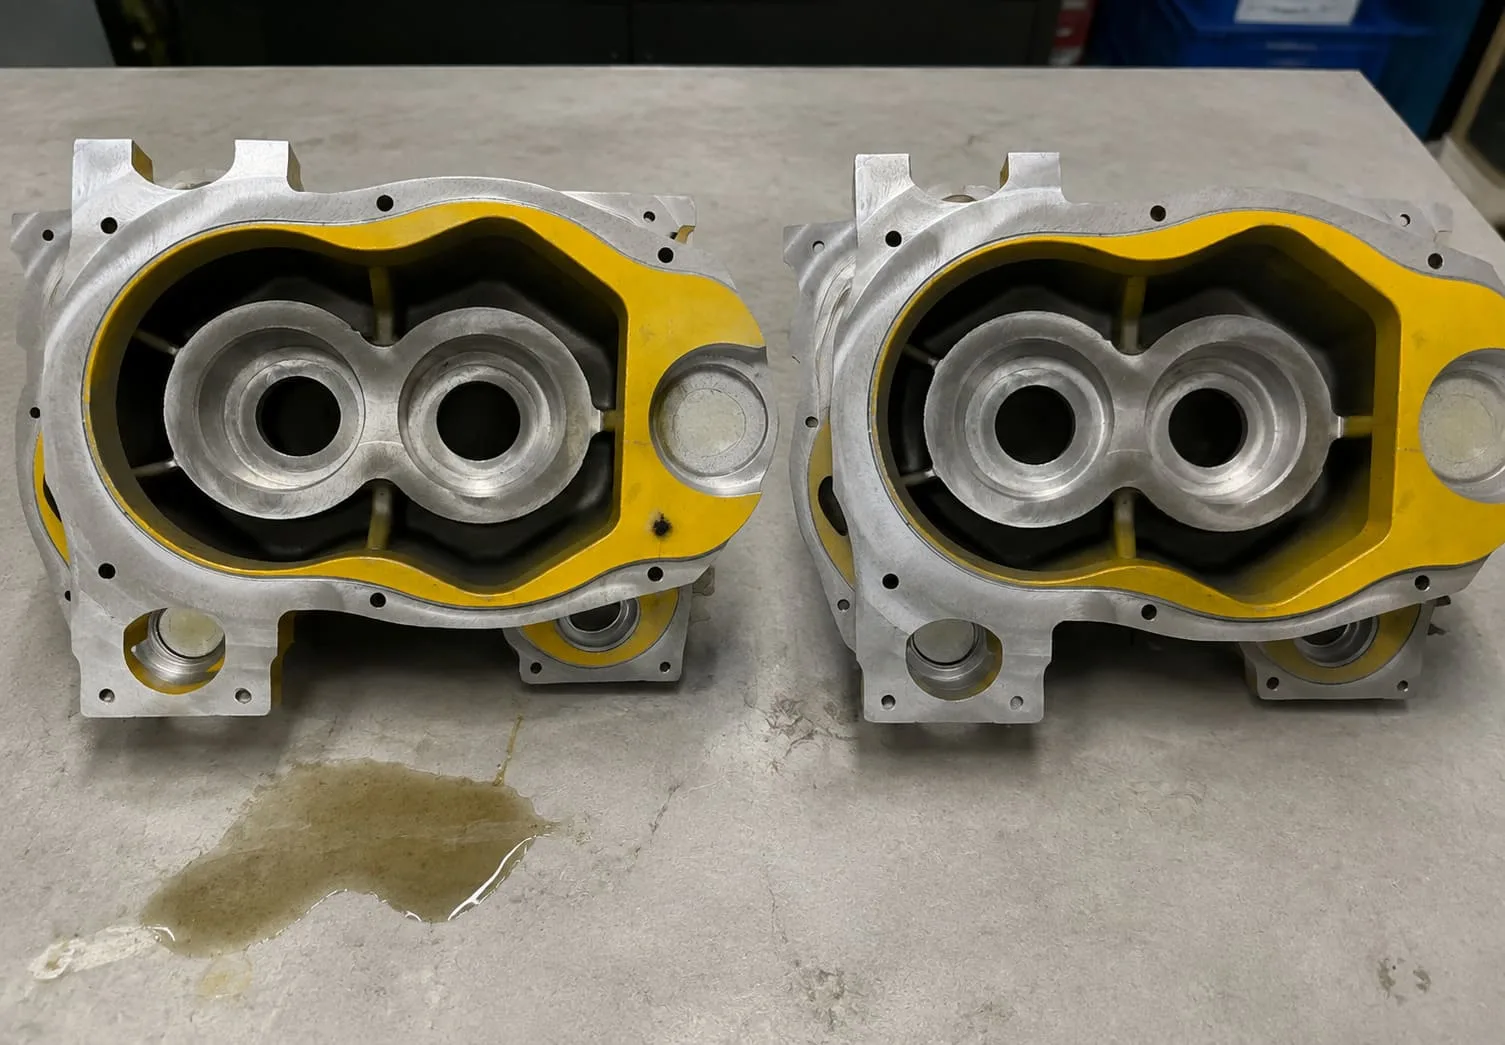
Anonymized evidence supplied during the first-batch leakage investigation.
Manufacturing response
The corrective route combined a customer-approved change from GAlSi9Cu3 to A356 with renewed sampling and review of the casting and finishing sequence. Attention was directed to local fill and solidification behavior, machined interfaces and the leakage-sensitive area.
Material substitution was only one part of the response. The revised route also used controlled production, dimensional verification and project-specific internal-integrity evaluation before release.
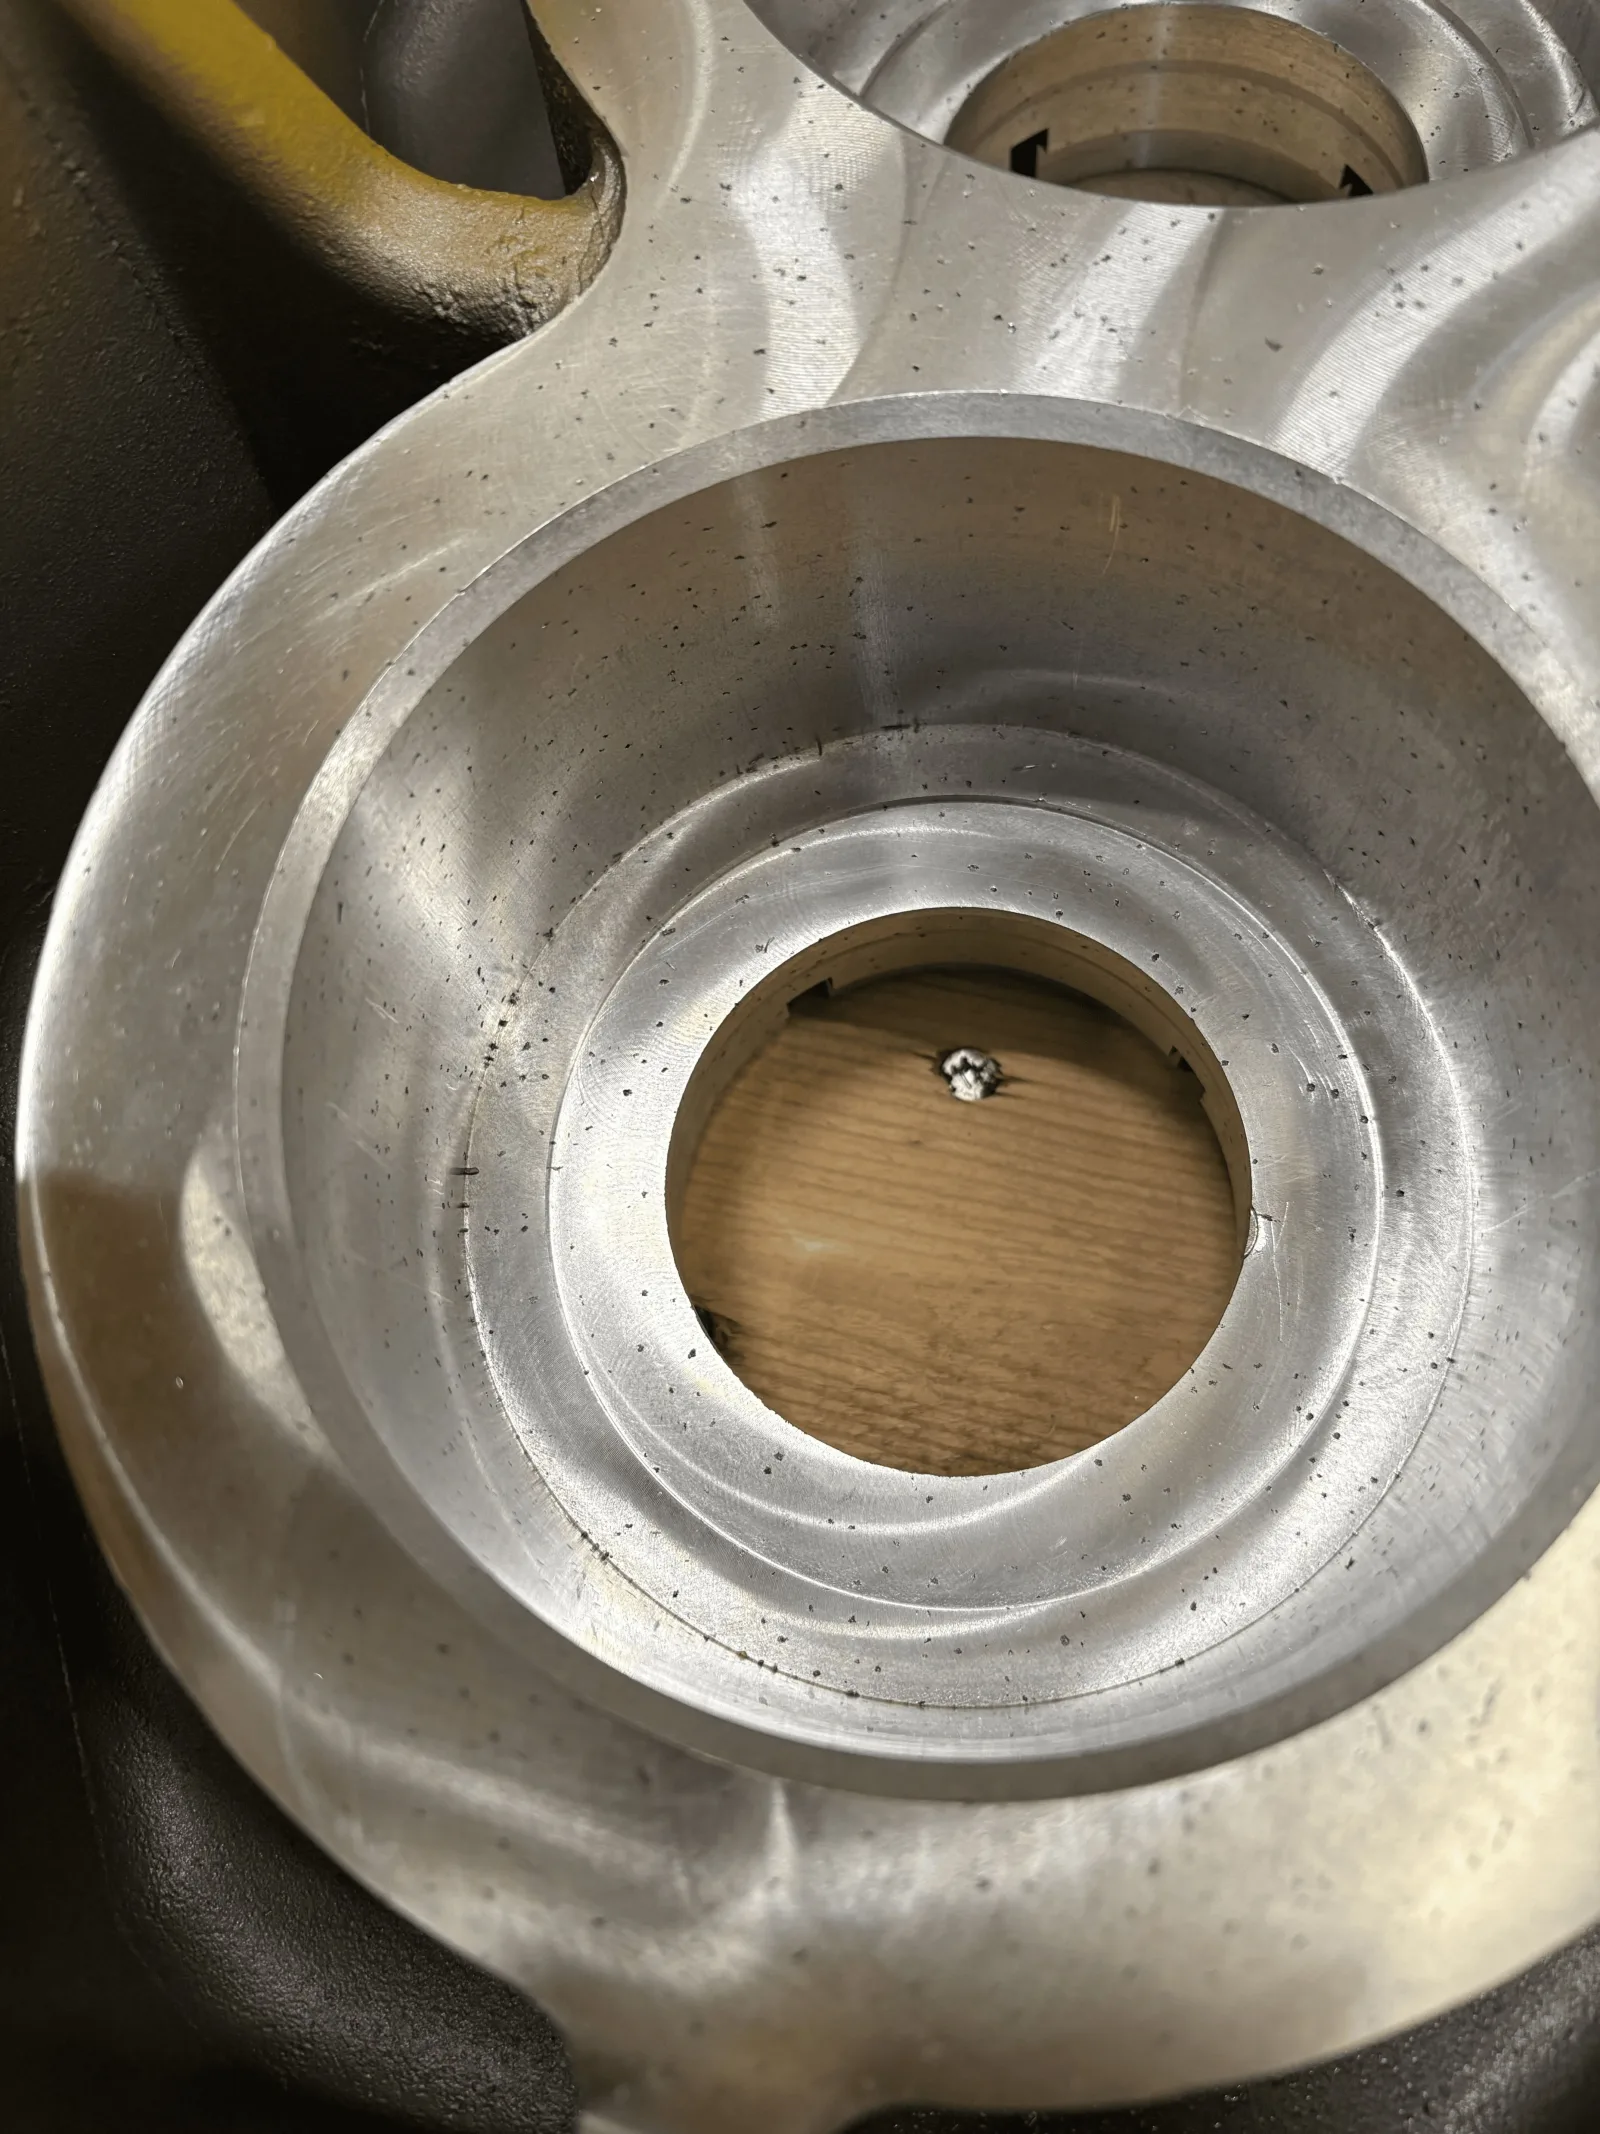
Investigation-stage evidence showing why visual inspection alone was not sufficient.
Verification and outcome
The project record states that the revised samples passed the defined checks and production continued under the optimized route, followed by repeat quarterly orders. This is a project-specific recovery case, not a claim of universal zero porosity or guaranteed pressure tightness.