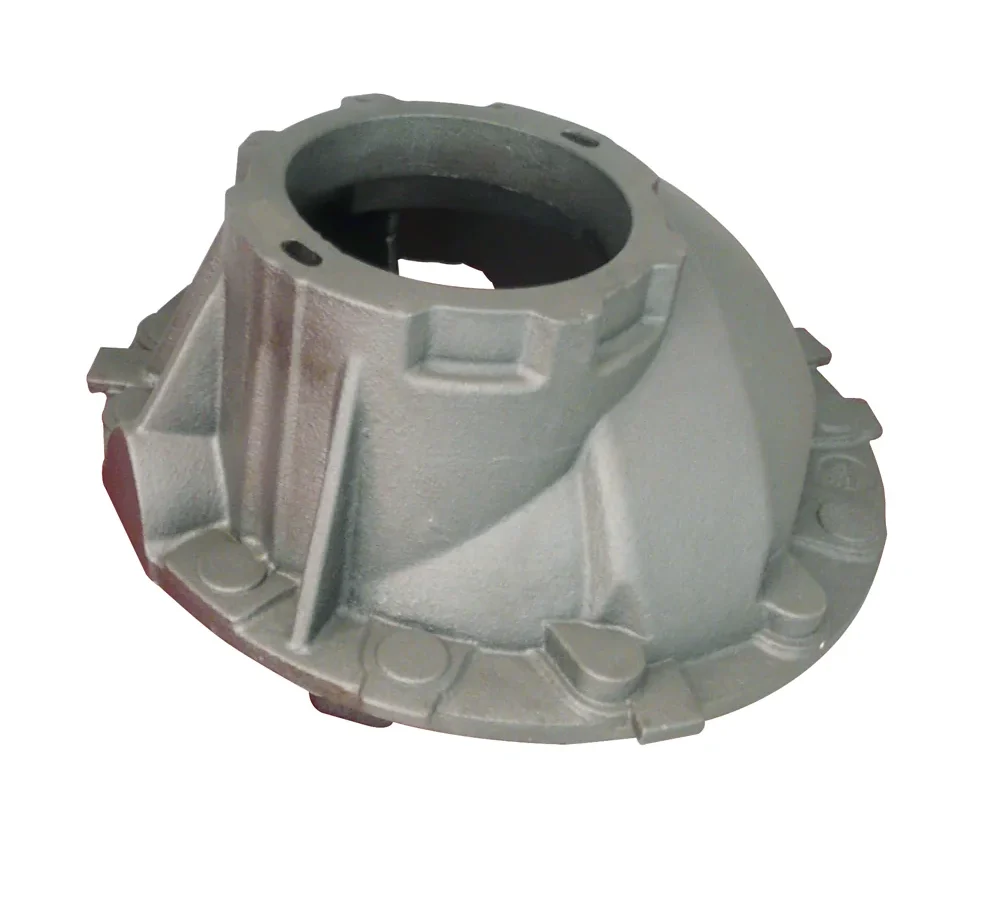
Part and application
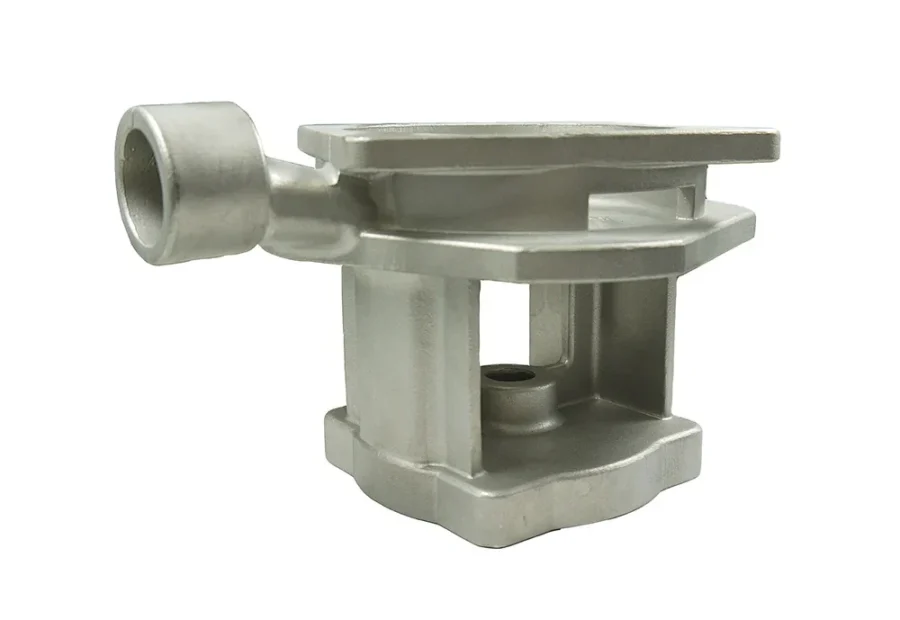
This HT250 cast-iron housing connects a pump body to its drive-side assembly and provides space for sealing components. A large circular flange, a surrounding ring of bolt bosses and an internal stepped cavity define the assembly geometry. The casting was produced in resin-sand molds and then machined at the functional interfaces.
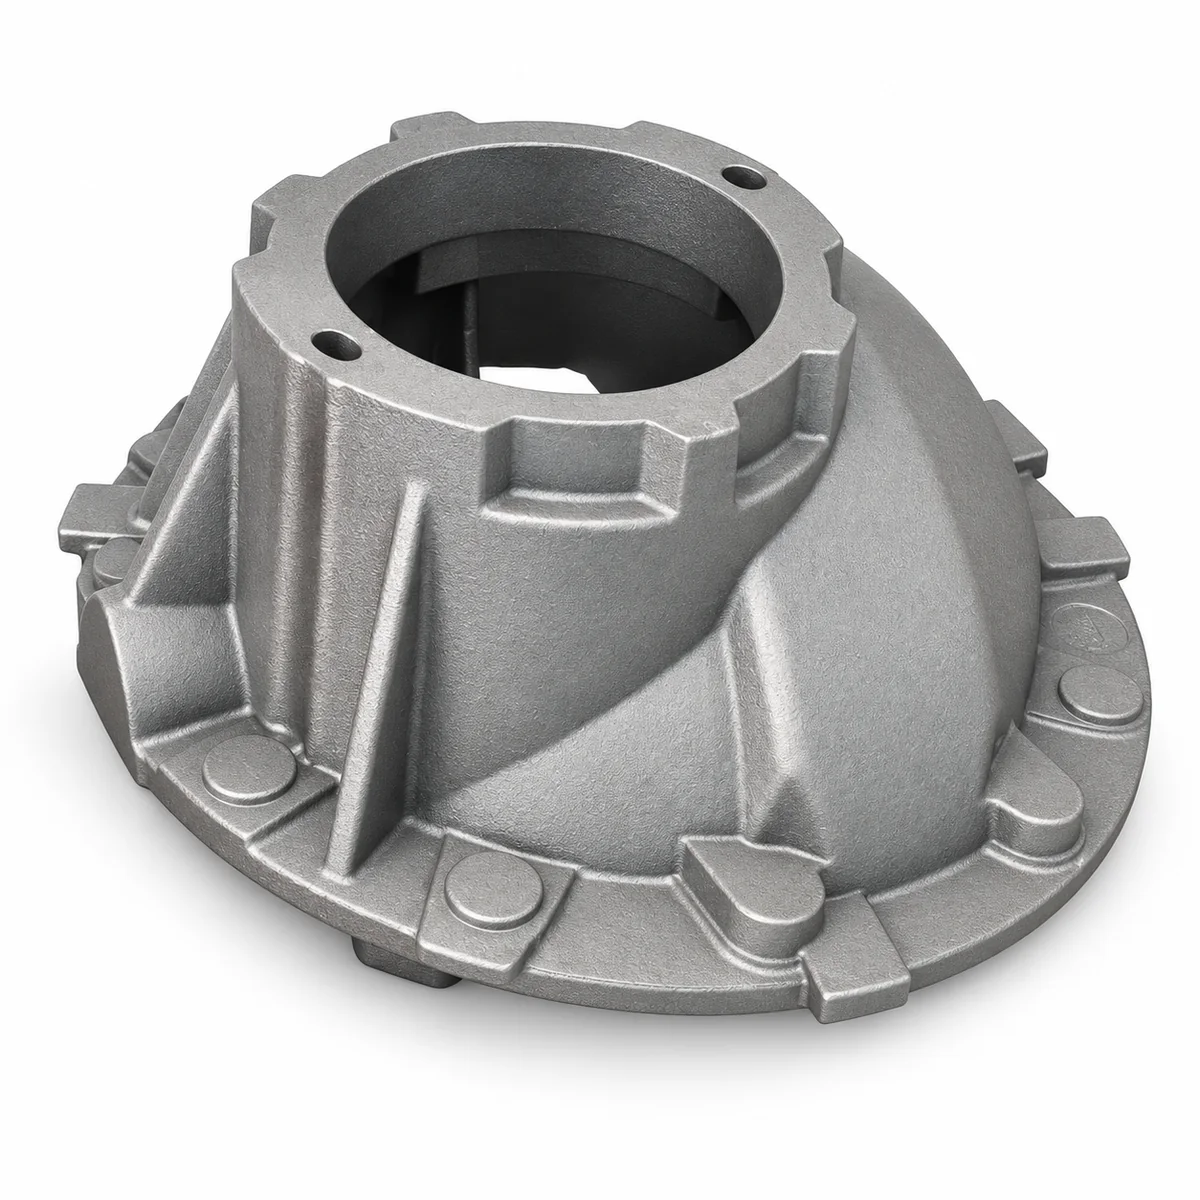
Customer requirements
The customer required a flat large flange, a casting without unacceptable cracks or shrinkage, and reliable interchangeability during assembly. The flange face, bolt holes and stepped bore were the main CNC features. The project specified 0.06 mm flange-face flatness and an IT8 bore.
Problem encountered
The broad flange tended to warp during production. Its diameter and comparatively thin section made it sensitive to casting stress and clamping pressure. If movement remained after machining, the pump-to-drive connection could lose its intended fit.
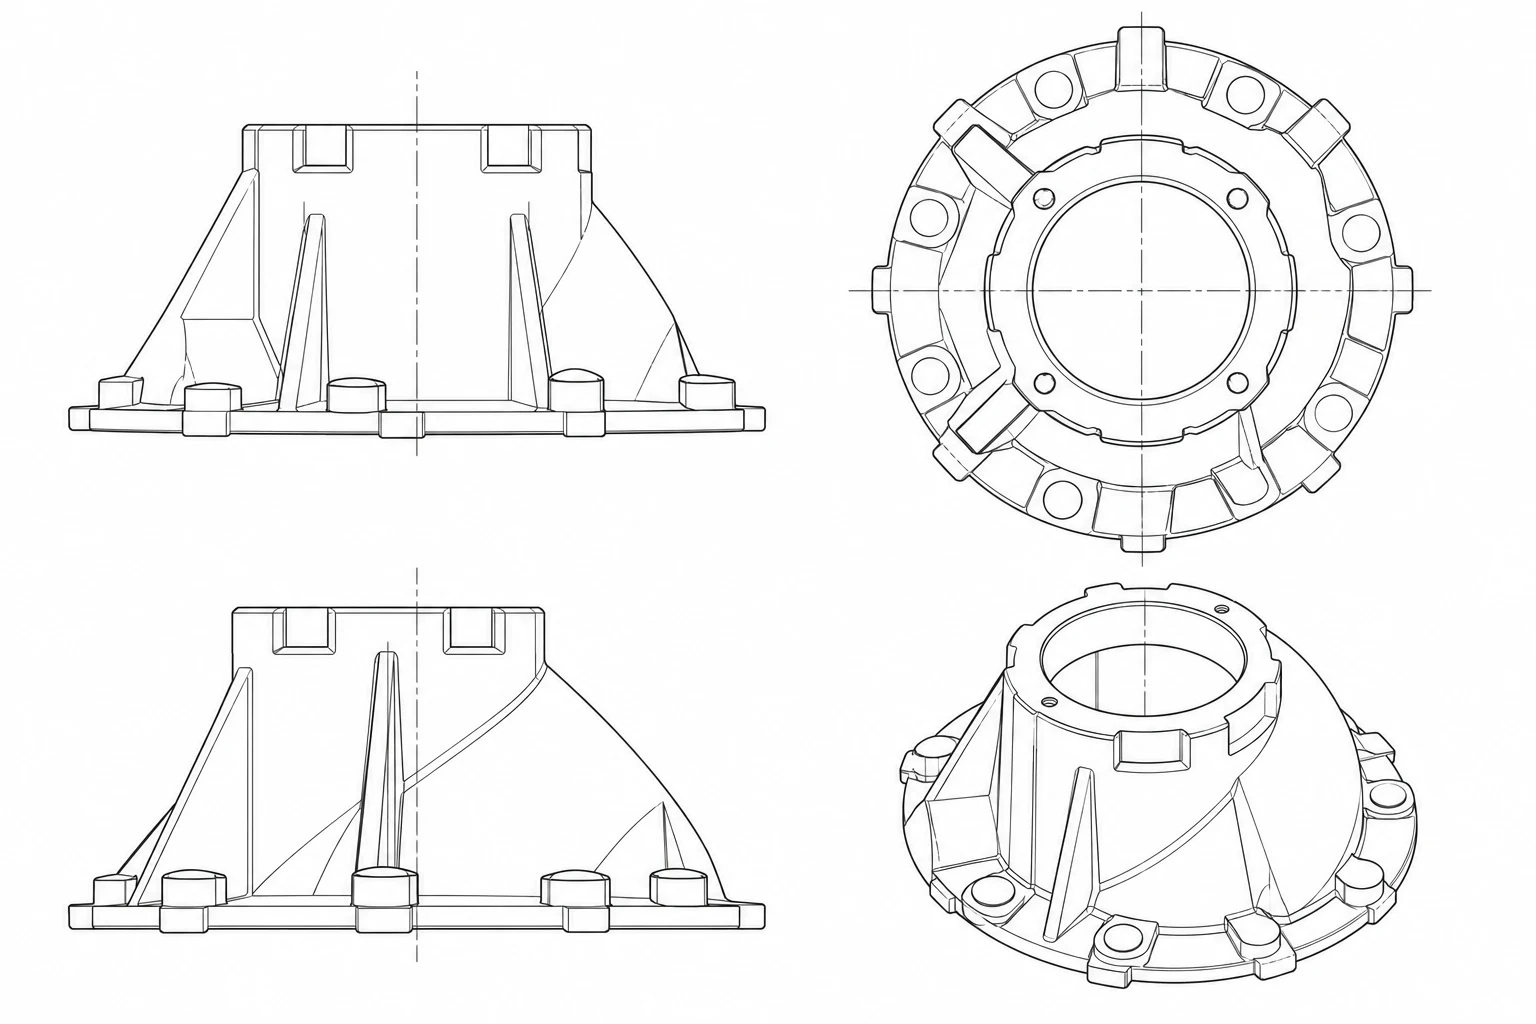
Process changes
The casting design was revised at relevant fillet transitions, and the natural aging period was extended before final machining. Resin-sand molding, core making, iron pouring, knockout, cleaning and shot blasting formed the production route. Machining then established the flange plane, bolt pattern and stepped bore.
Inspection
The inspection route listed material testing, CMM dimensional checks and visual examination. Checks focused on the large flange plane, bore and other assembly dimensions after machining.
Reported project result
The supplied project record says flange deformation was brought within the specified tolerance and the housing entered batch delivery. The acceptance limit was specific to this part.