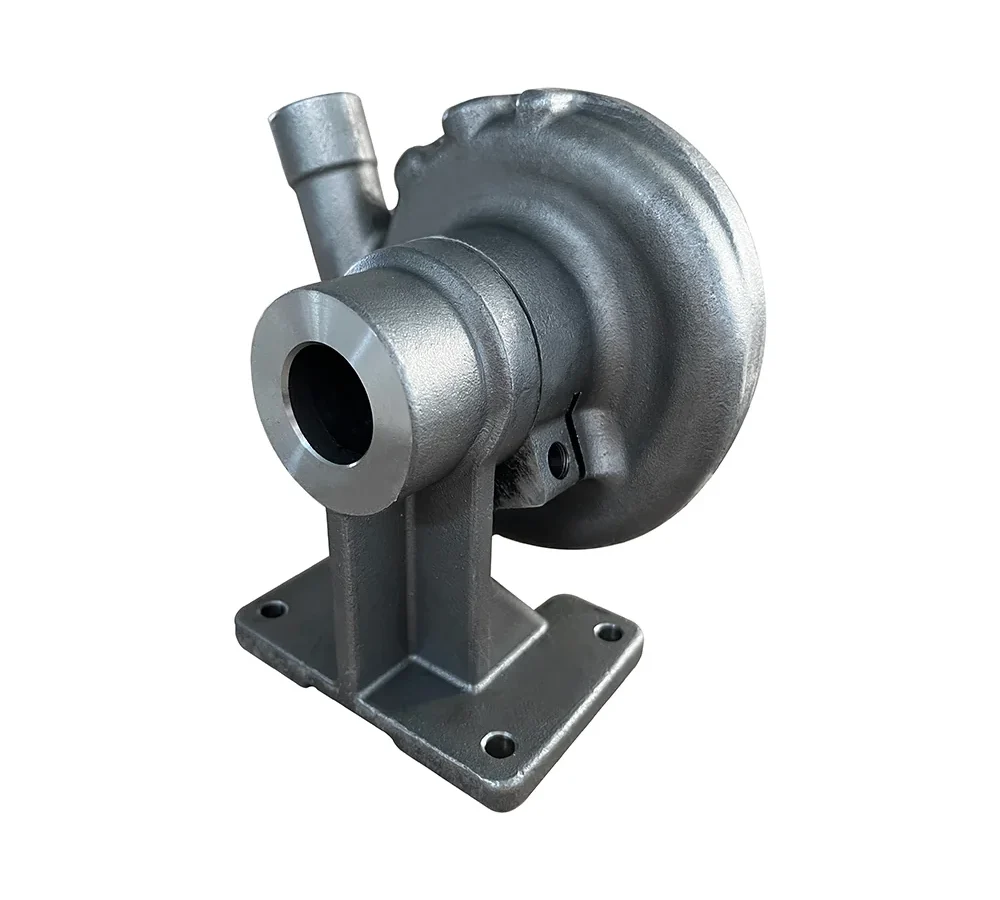
Part and application
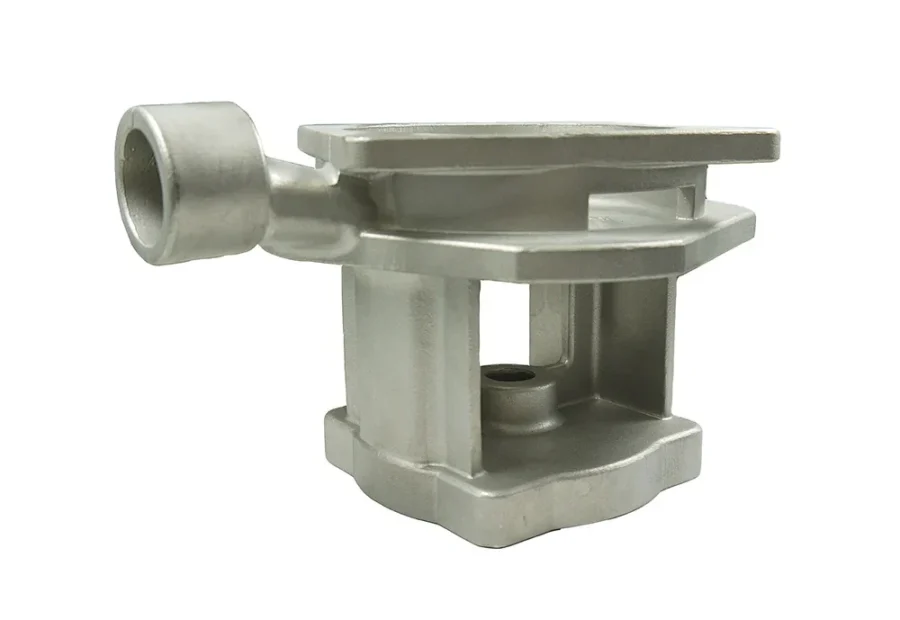
This HT200 gray-iron casing is a small centrifugal pump body with a volute, side inlet, upper outlet and integral mounting foot. Ribs join the casing to the base. The project used resin-sand casting followed by cleaning, shot blasting and CNC work on the pump and base interfaces.
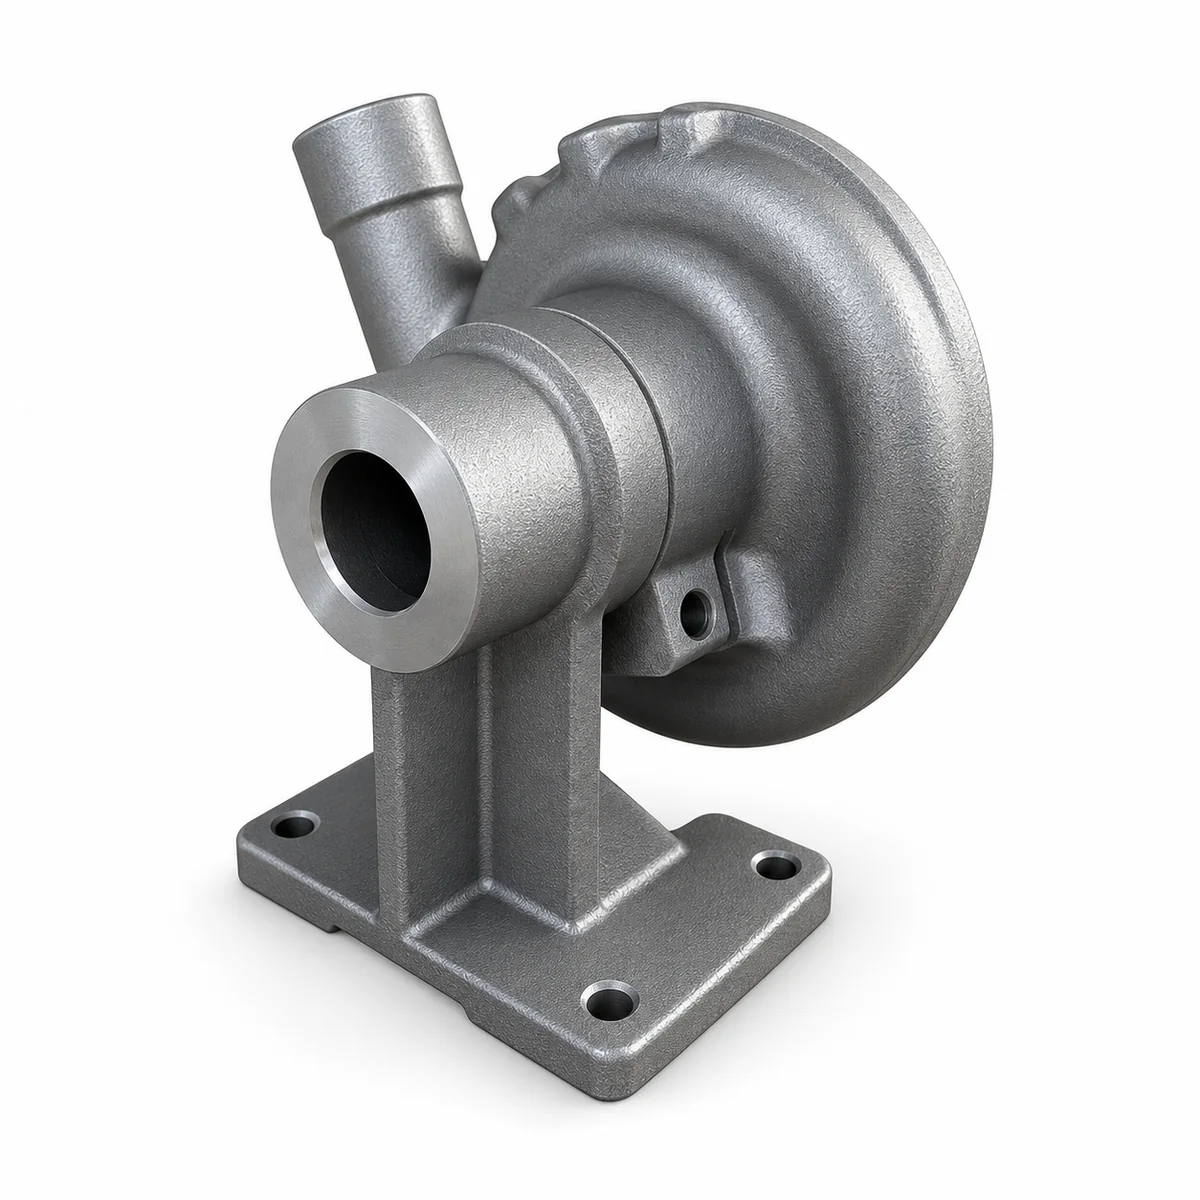
Customer requirements
The customer required a sound casting, a flat base plane and interchangeability during pump assembly. The inlet bore, outlet end face, base mounting plane and locating face were identified as machined features. The project specified register roundness of 0.05 mm or better.
Problem encountered
Gas pores appeared where the base ribs join the pump body. This local geometry affected both casting appearance and the soundness needed near the mounting structure. The difference in height between the base and volute also complicated a single machining setup.
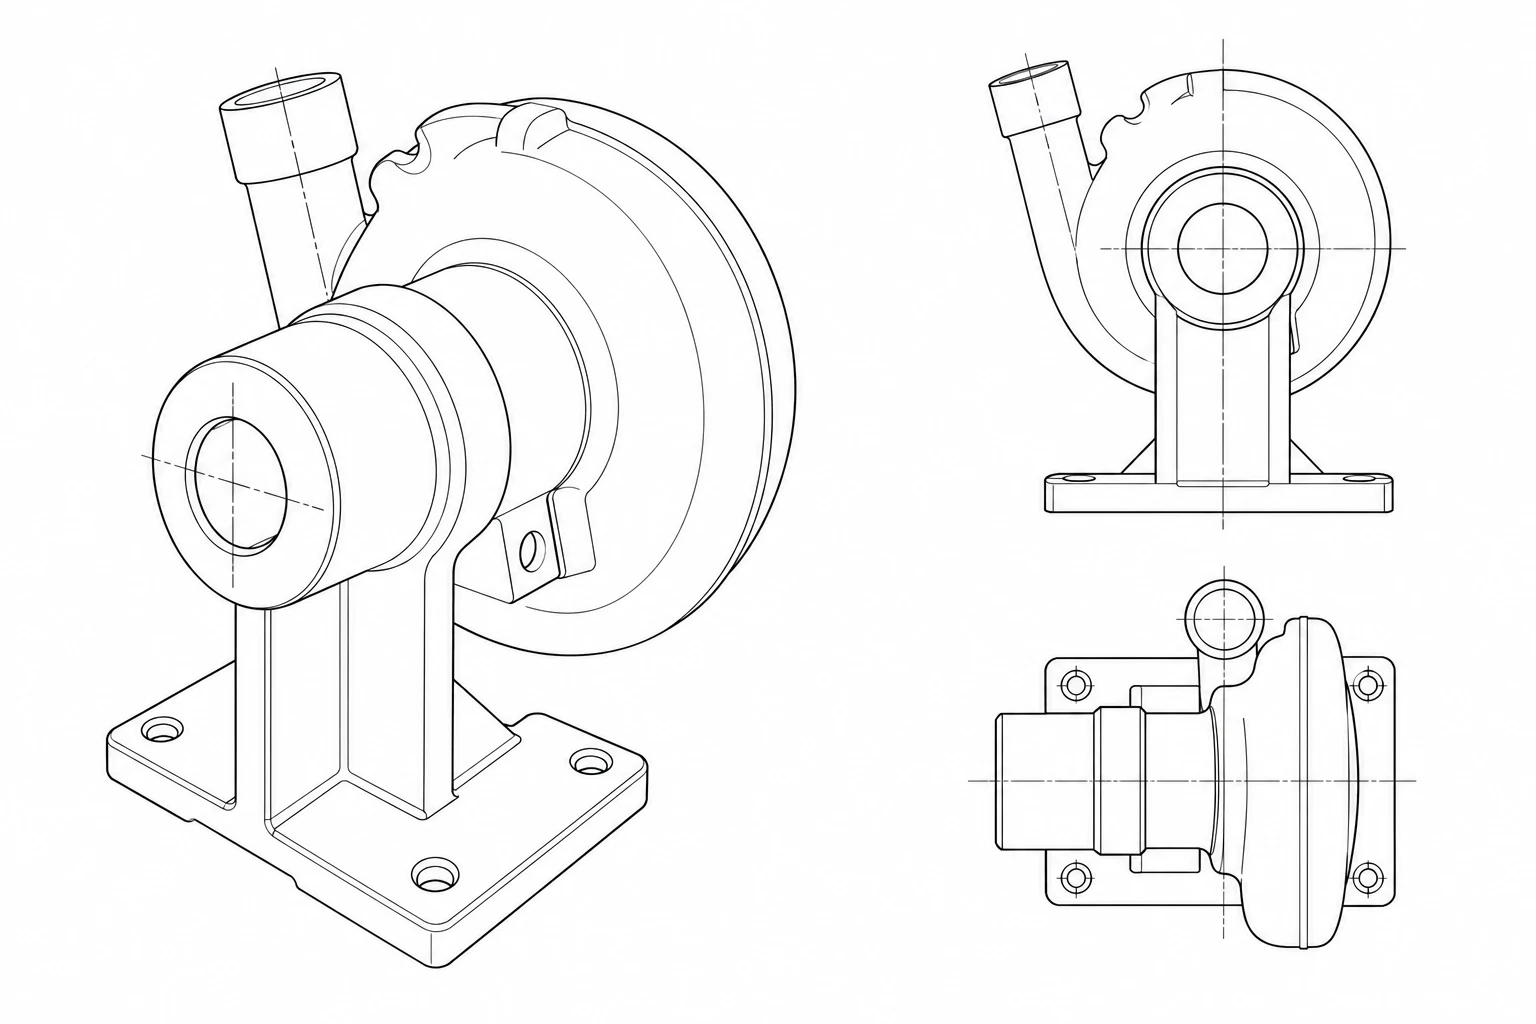
Process changes
The foundry added a vent path in the rib area and adjusted pouring rate to improve gas escape during filling. After knockout, flash cleaning and shot blasting, the casting proceeded to machining of the inlet, outlet, base and locating face.
Inspection and pressure test
Material analysis, dimensional checks, visual inspection and hydrostatic testing were part of the project inspection route. The supplied record reports no leakage at 0.4 MPa.
Reported project result
The source record describes the rib-area defect as controlled and the part as released for batch delivery. That result applies to this pump casing and does not replace pressure or dimensional testing on other designs.