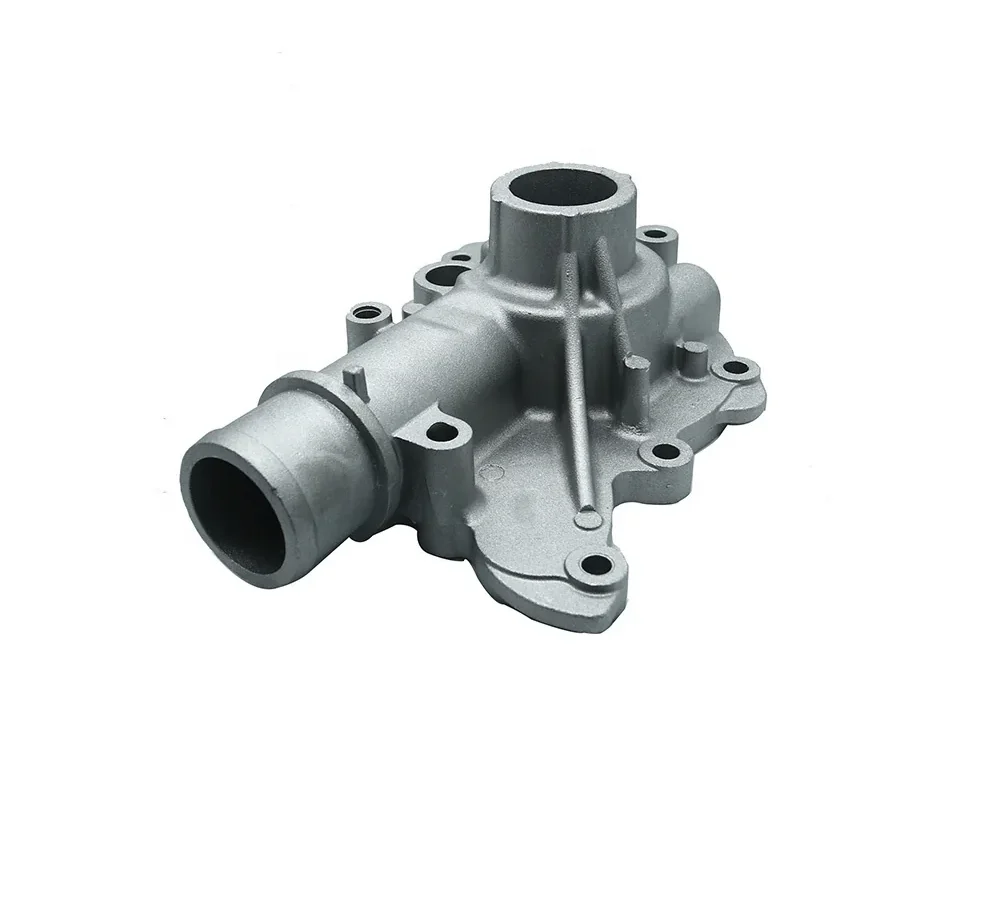
Part and application
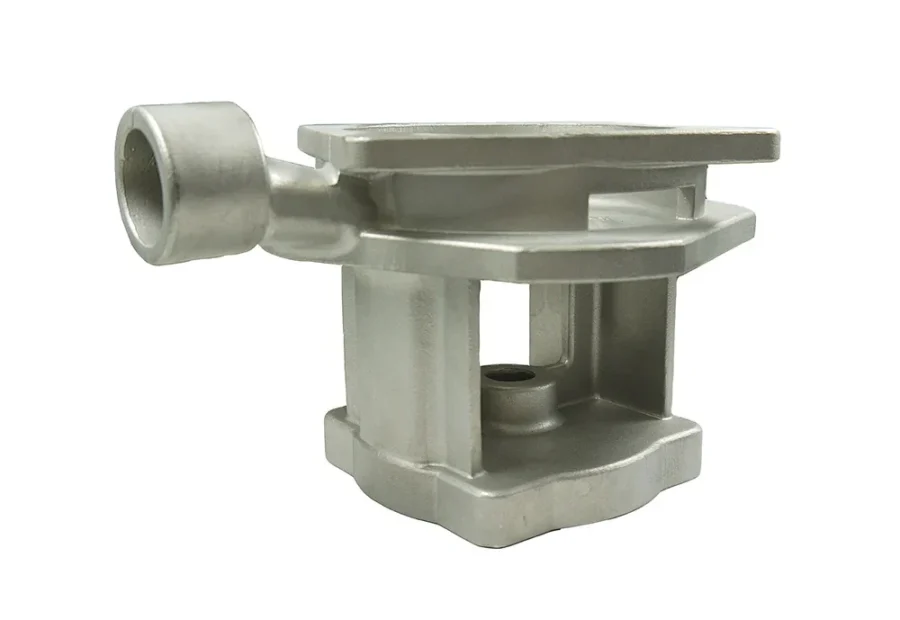
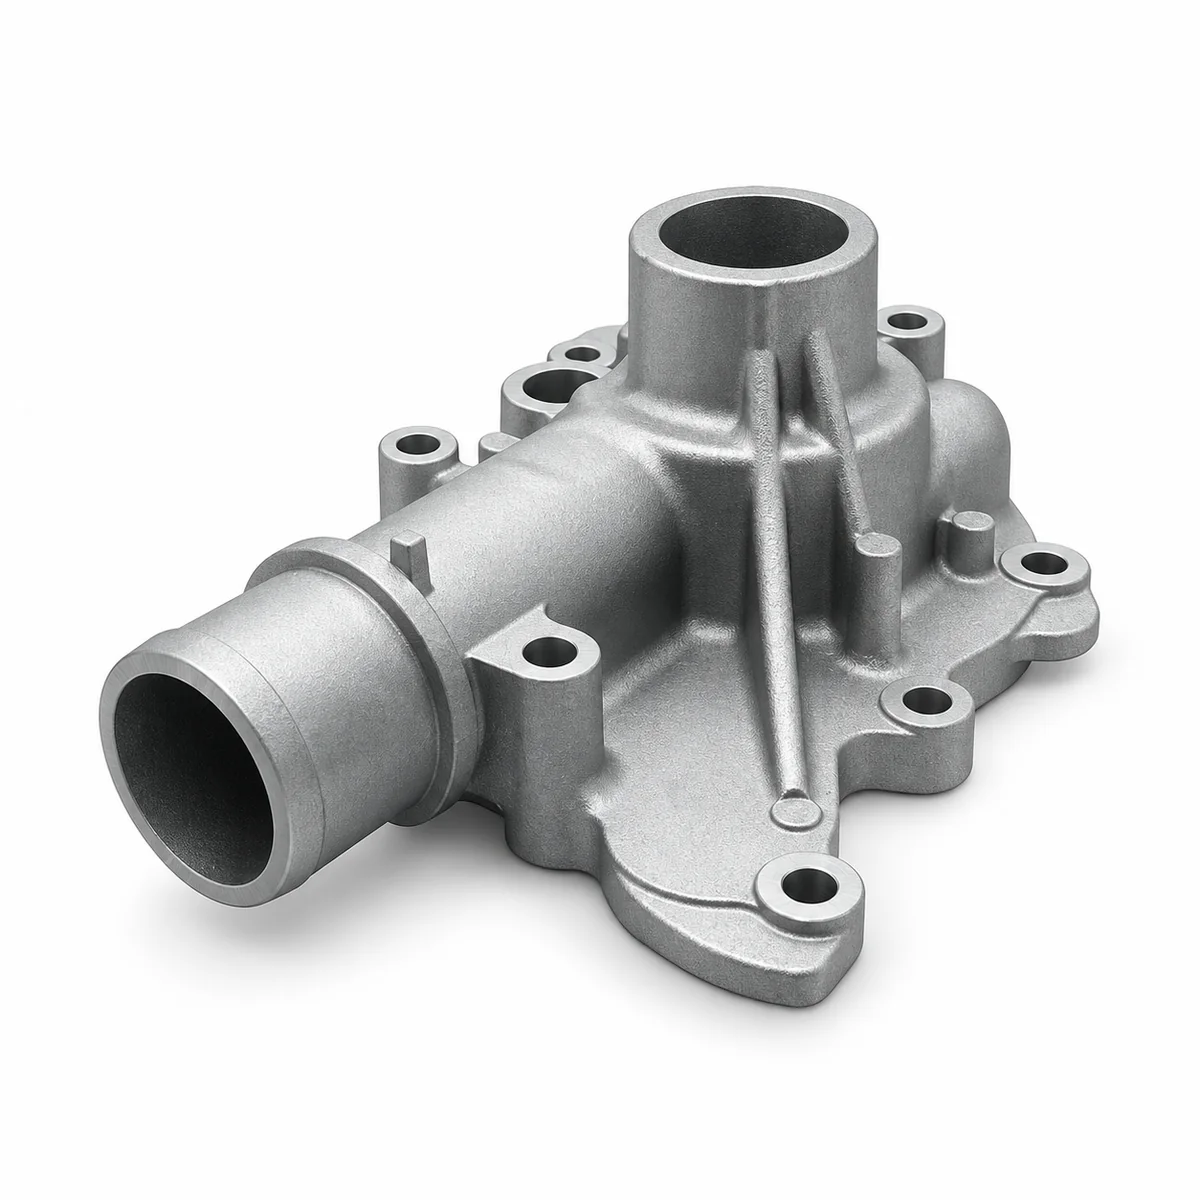
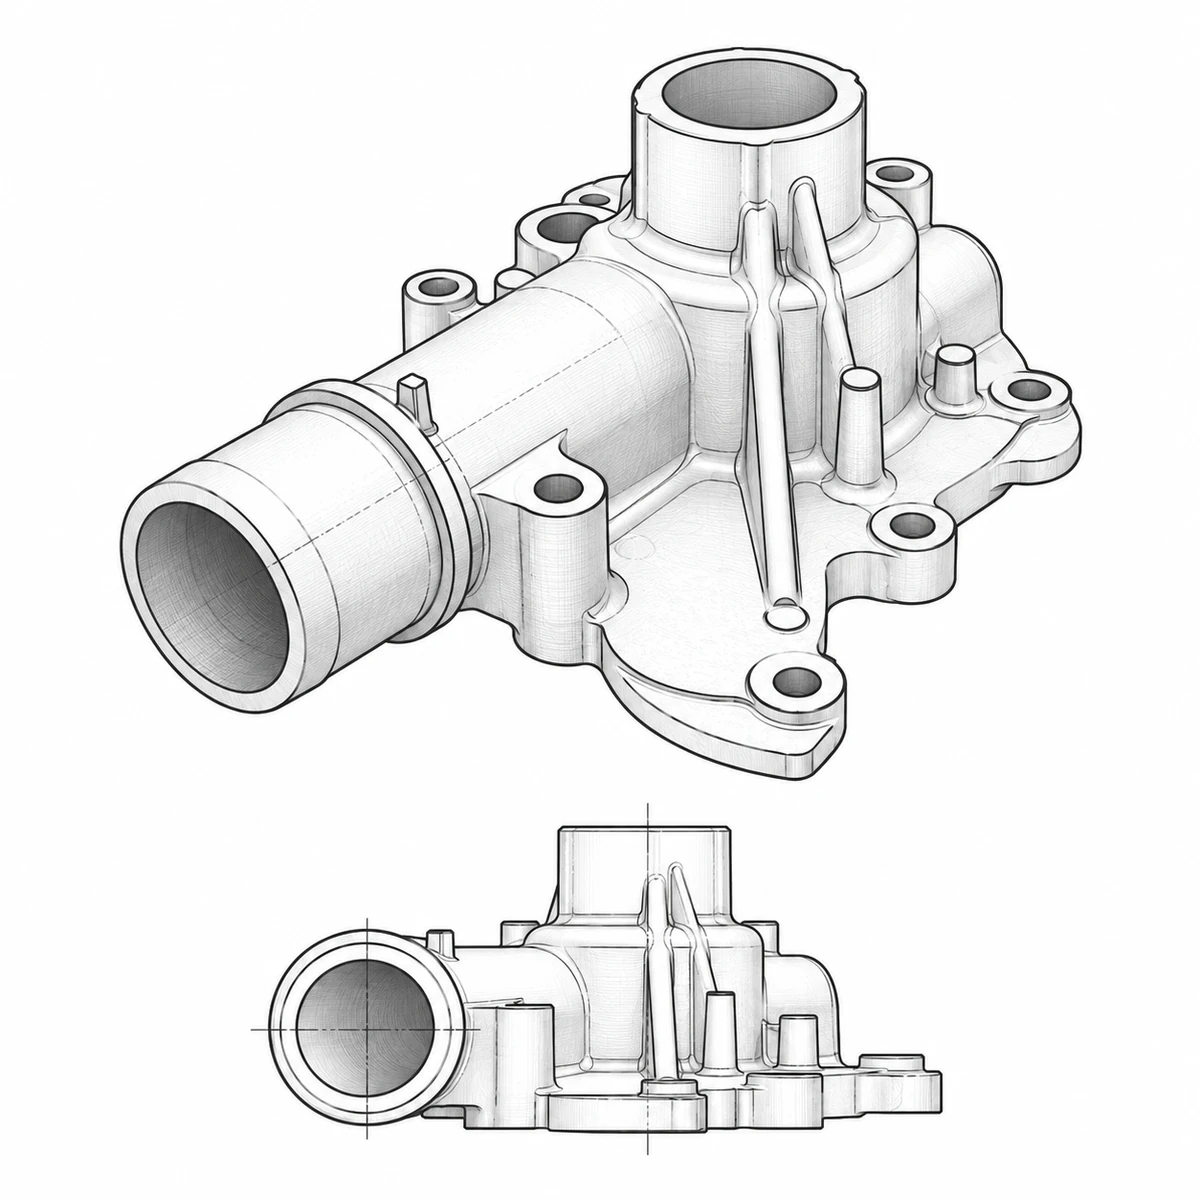
This compact A356 aluminum housing forms the cooling-water chamber of a small engine pump. Integrated inlet and outlet connections, closely spaced mounting bosses and ribs place thin sections next to heavier features. The part was made by metal-mold gravity casting and received T6 treatment before finishing.
Customer requirements
The customer needed consistent assembly dimensions, a sound coolant passage and a casting free of unacceptable gas pores or leakage. The bearing-seat bore, pipe faces, mounting flange and bolt holes required CNC machining. The project specified an IT7 bearing bore and ±0.04 mm hole-position control.
Problem encountered
Cold shuts appeared in a thin-wall region during development. The thin section increased the risk of incomplete filling during gravity casting. Thin walls also made the part sensitive to vibration during high-speed machining.
Process changes
The mold temperature was raised and the gate design revised to improve filling of the thin section. After gravity pouring, the castings were cooled, removed from the mold, deburred and blasted. The specified T6 treatment and CNC finishing followed the casting stage.
Inspection and pressure test
The inspection plan included spectrometer material checks, caliper and CMM dimensional measurements, visual review and hydrostatic leak testing. The supplied test result records no leakage at 0.3 MPa after a 3-minute hold.
Reported project result
The source record reports a substantial reduction in cold-shut defects and stable batch delivery after the mold and gate changes.