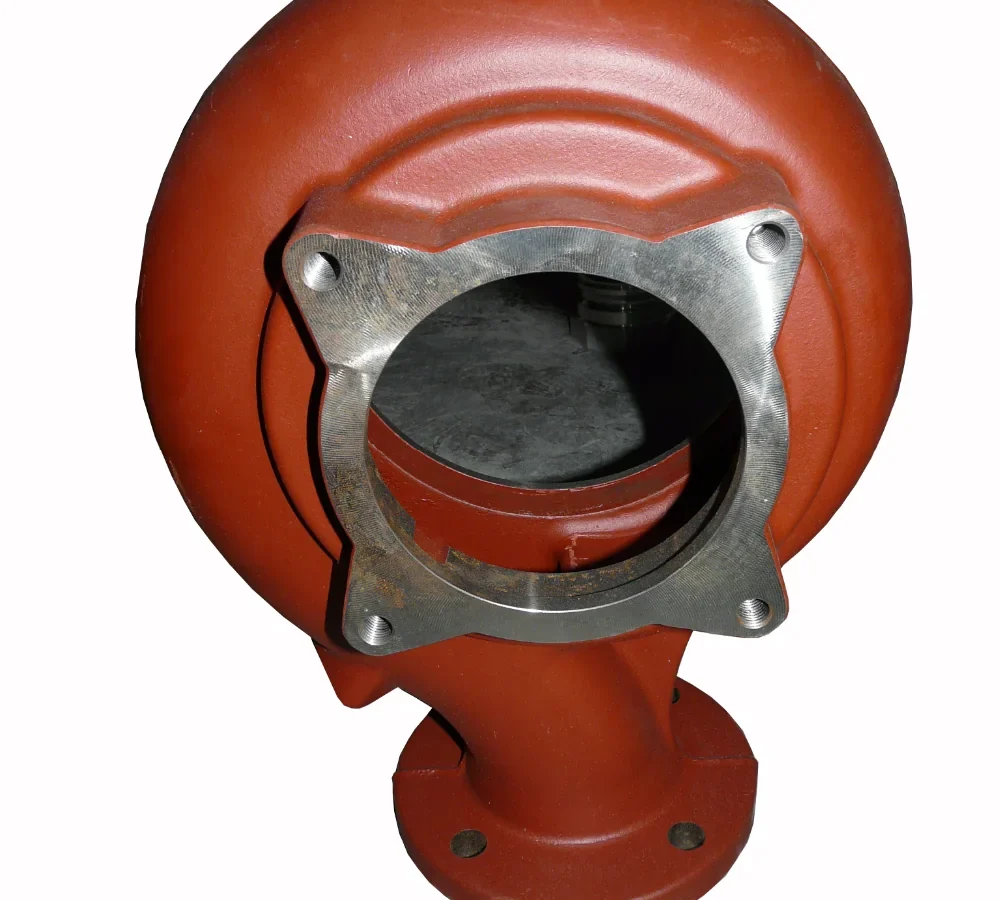
Part and application
The HT200 cast-iron volute forms the main flow casing of an industrial centrifugal pump. Its spiral chamber guides the liquid toward the outlet, while integrated inlet and discharge flanges provide assembly and sealing interfaces. The casing was produced by resin-sand casting, with the internal flow passage formed by sand tooling and subsequent cleaning.
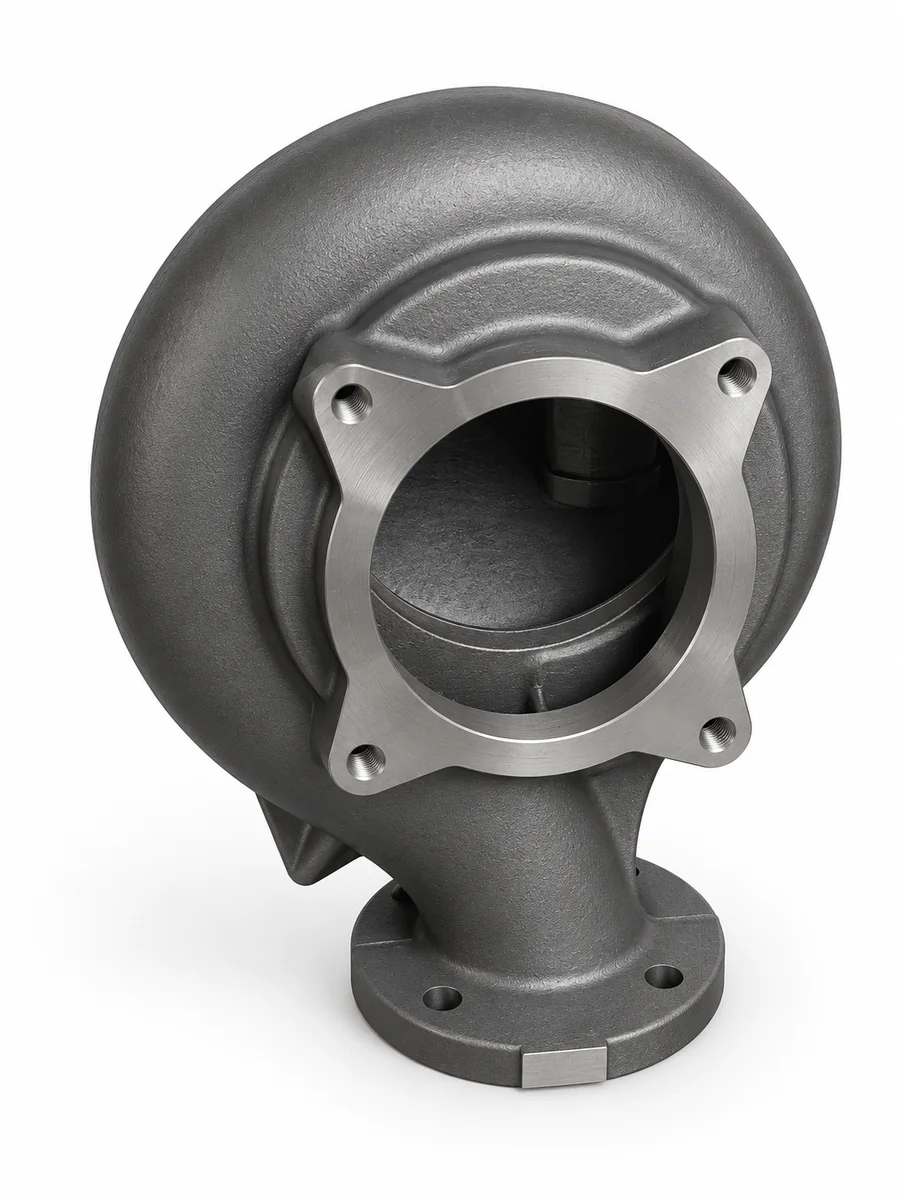
Customer requirements
The pump manufacturer required a clean curved passage, a sound pressure boundary and flange faces without unacceptable casting defects. The flange sealing planes, bolt holes and locating surfaces were scheduled for CNC finishing. The project specified 0.06 mm flange-face flatness and Ra 3.2 μm on the sealing face after machining.
Problem encountered
Sand adhered to the curved inner wall of the volute during casting. The shape made that area difficult to reach during cleaning. Remaining bonded sand would compromise the specified internal surface and create additional rework before pressure testing and pump assembly.
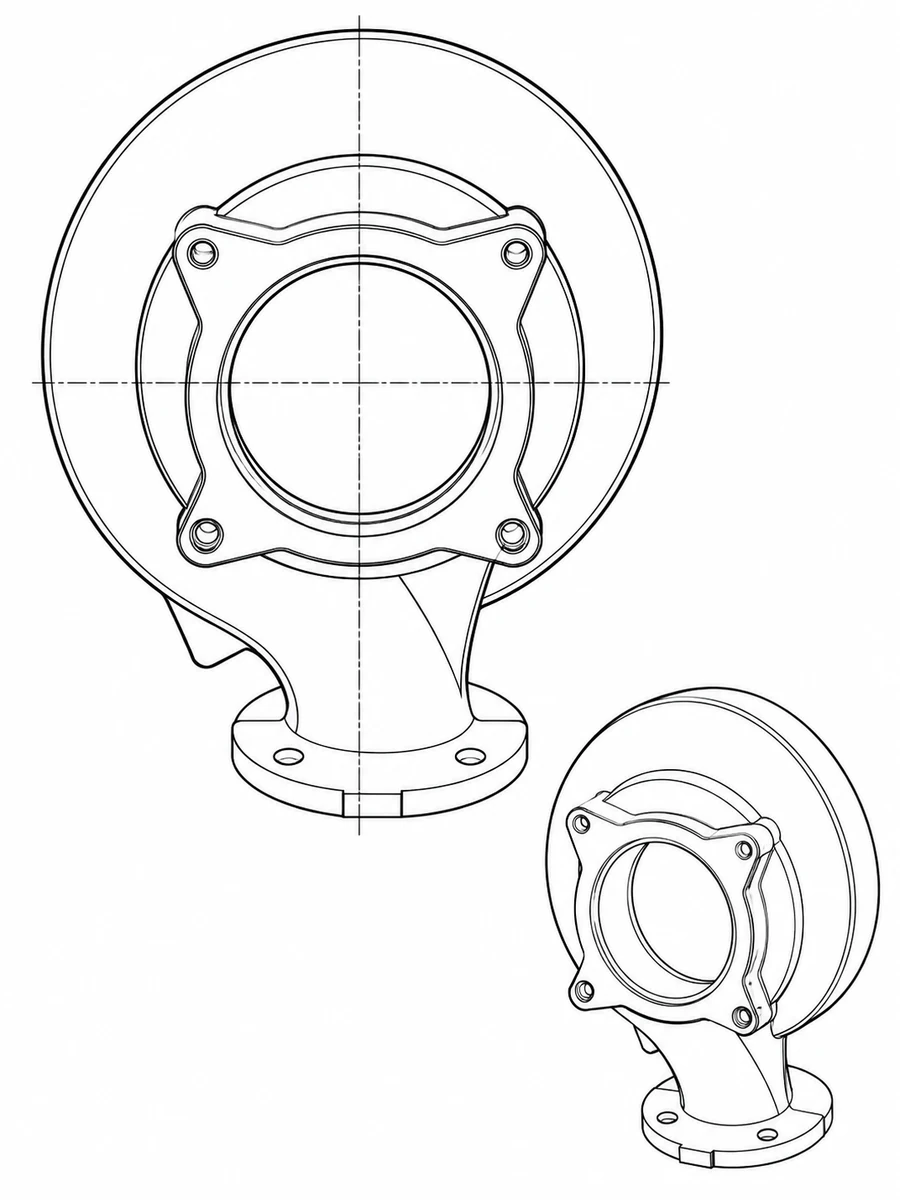
Process changes
A high-temperature refractory coating was applied to the relevant mold surfaces, and sand-mold compaction was adjusted to improve the face in contact with the curved passage. The casting route then continued through pouring, knockout, cleaning and grinding. The inlet and outlet flange faces and locating features were machined after the passage was cleaned.
Inspection and pressure test
The project inspection route covered material analysis, dimensions, visual surface quality and hydrostatic pressure. The supplied test result records no leakage at 0.6 MPa after a 5-minute hold. The pressure value belongs to this project and is not a universal pump-casing rating.
Reported project result
The supplied record says the sand-adhesion issue improved and the casting met the pump manufacturer’s assembly requirement.