Part and application
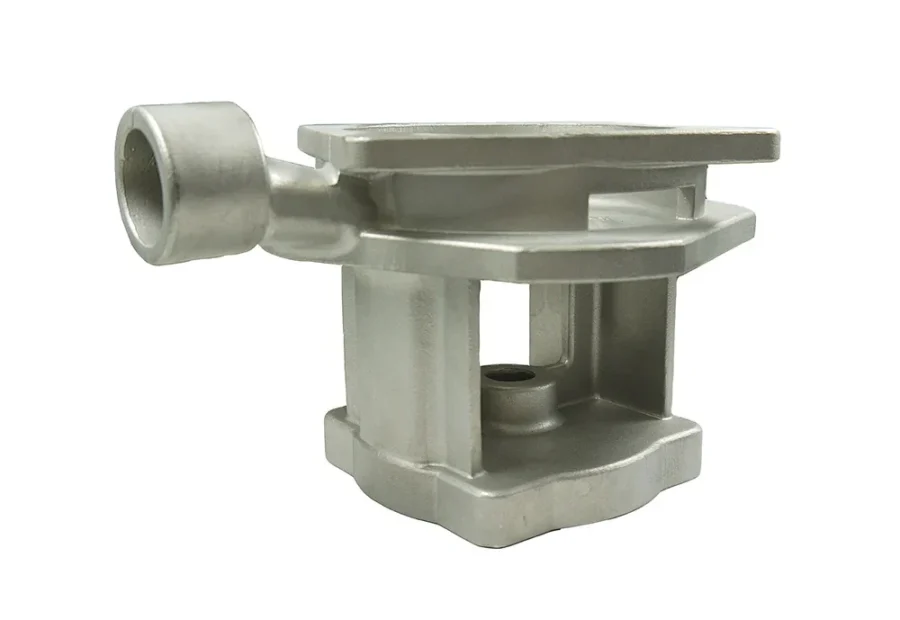
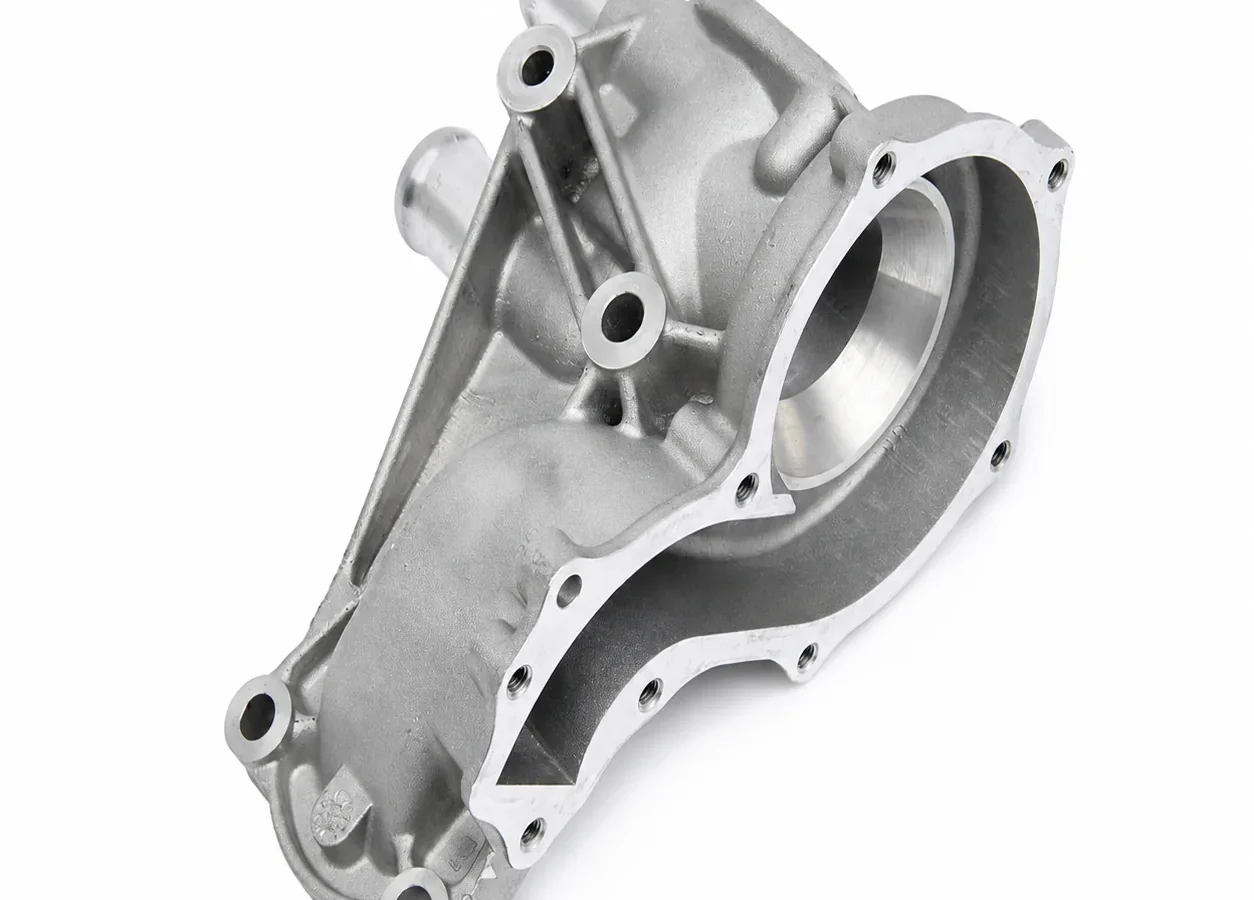
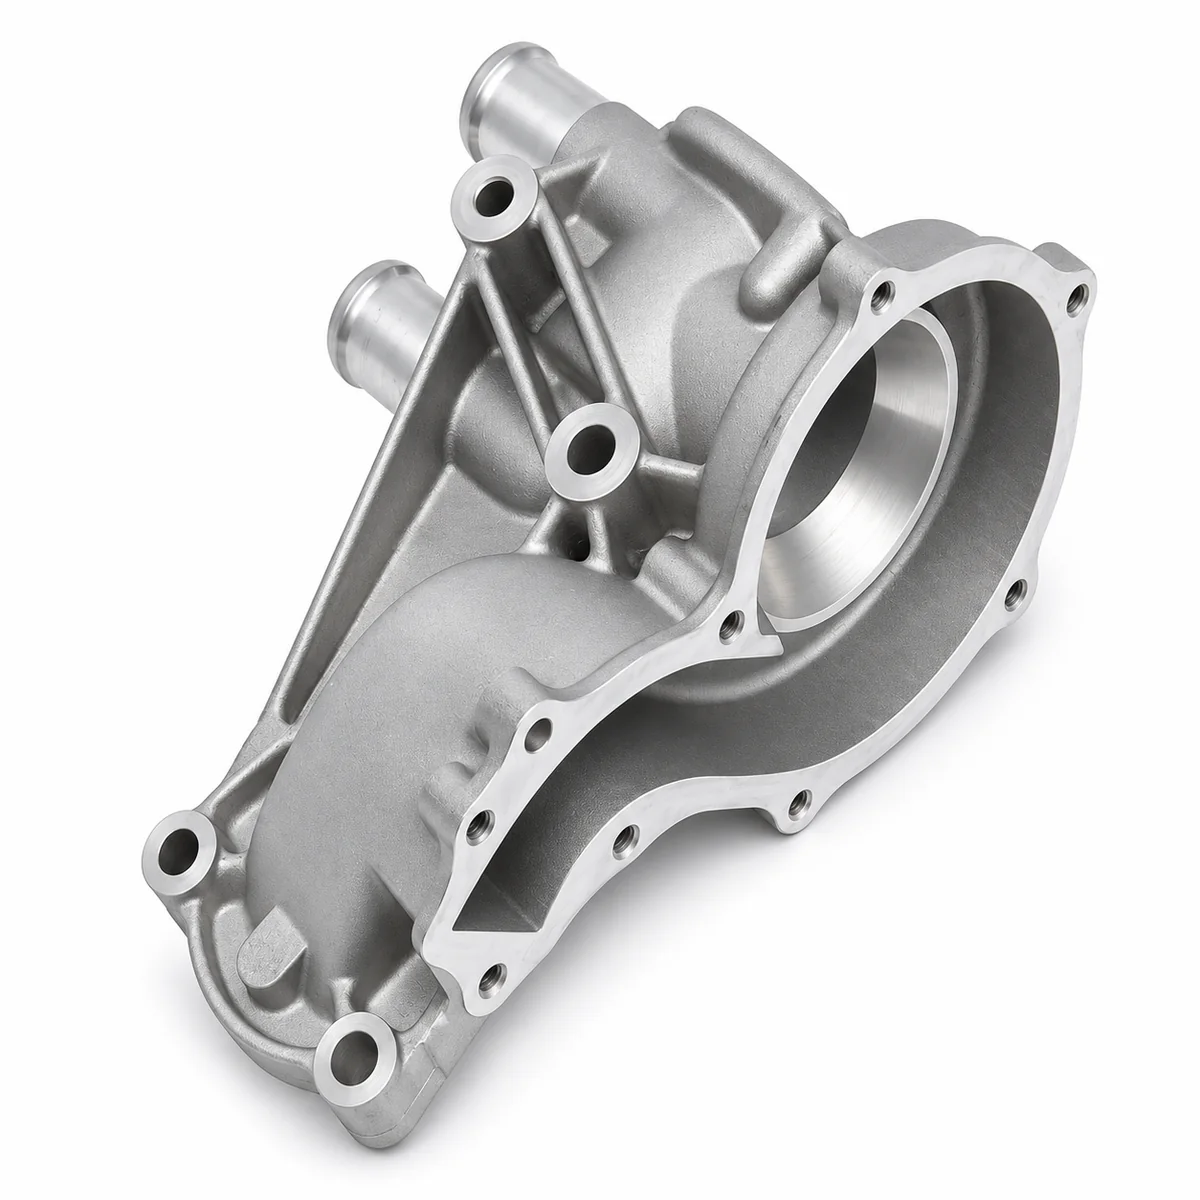
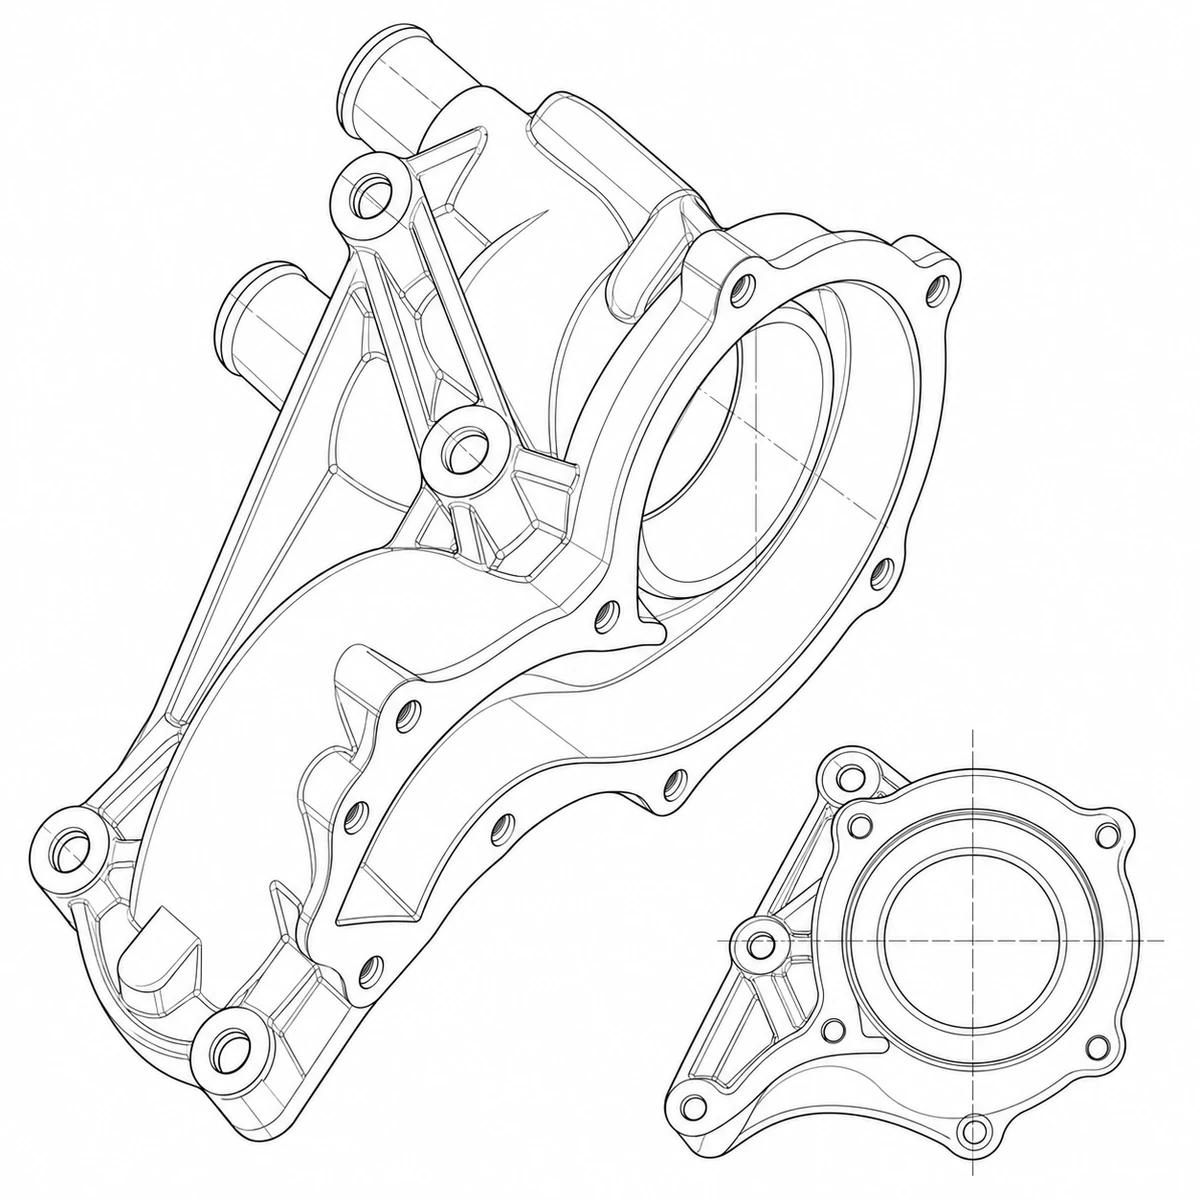
This A356.2 aluminum casting serves a heavy-vehicle engine water pump. It supports the pump shaft and seal assembly while forming the cooling-water passage. A large flange register, two water connections and a curved internal channel create several interfaces that must work together after machining. The project used a metal mold and gravity pouring, followed by T6 heat treatment.
Customer requirements
The customer required a smooth internal passage without unacceptable pores or surface defects, along with consistent assembly dimensions. The flange register, bearing bore, two water connections and bolt holes were assigned to CNC machining. The project specified register roundness at or below 0.04 mm and hole-position control of ±0.05 mm.
Problem encountered
The internal curved passage trapped gas during early production and produced porosity. The route also presented a fixture challenge: clamping the curved thin-wall casting for machining could distort the large flange and shift the critical interfaces.
Process changes
The vent-groove layout was revised and pouring speed adjusted to give gas a clearer escape route during gravity filling. After cooling and removal from the metal mold, the casting was trimmed and blasted. The machined register and connection faces were then checked against the assembly datums.
Inspection and pressure test
Material analysis, caliper and CMM dimensional checks, visual inspection and hydrostatic testing were listed for this project. The supplied record reports no leakage under a 0.35 MPa water-pressure test; no hold duration was stated in that record.
Reported project result
The supplied project record reports that the nonconforming rate fell to 1.2% after the venting and pouring adjustments, followed by stable supply. This is a result for this casting, not an expected rate for other water pump housings.