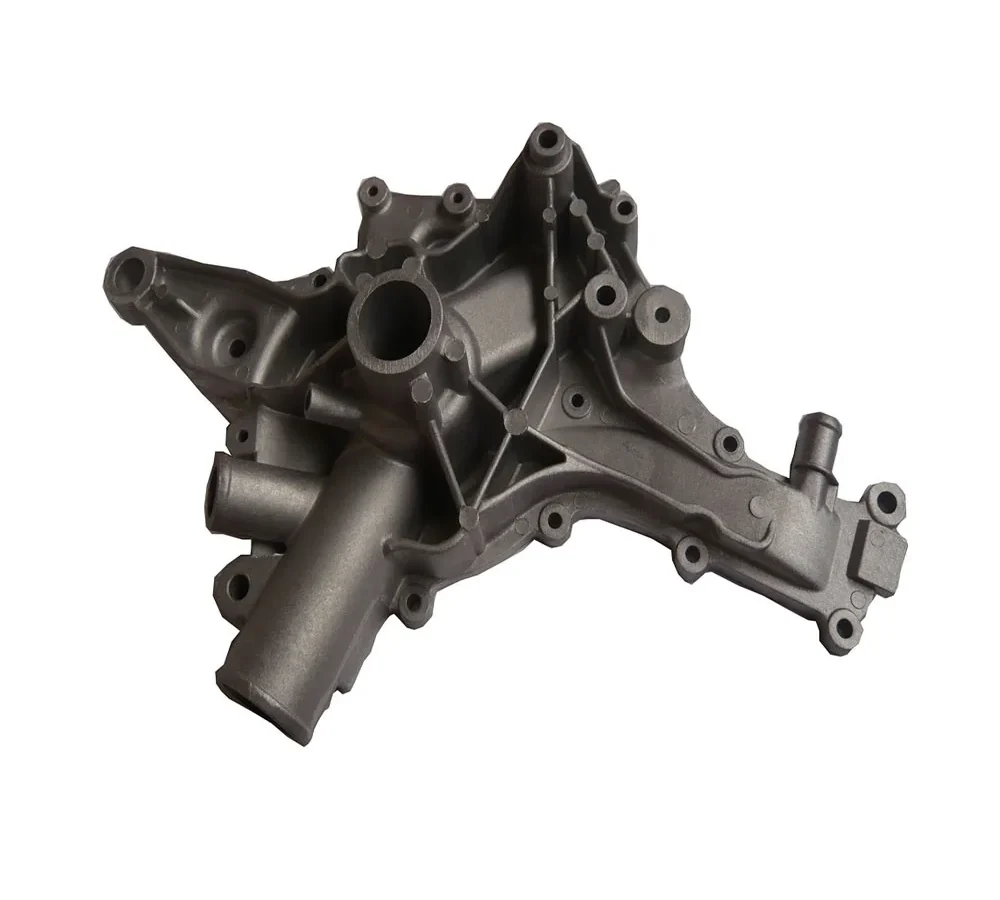
Part and application
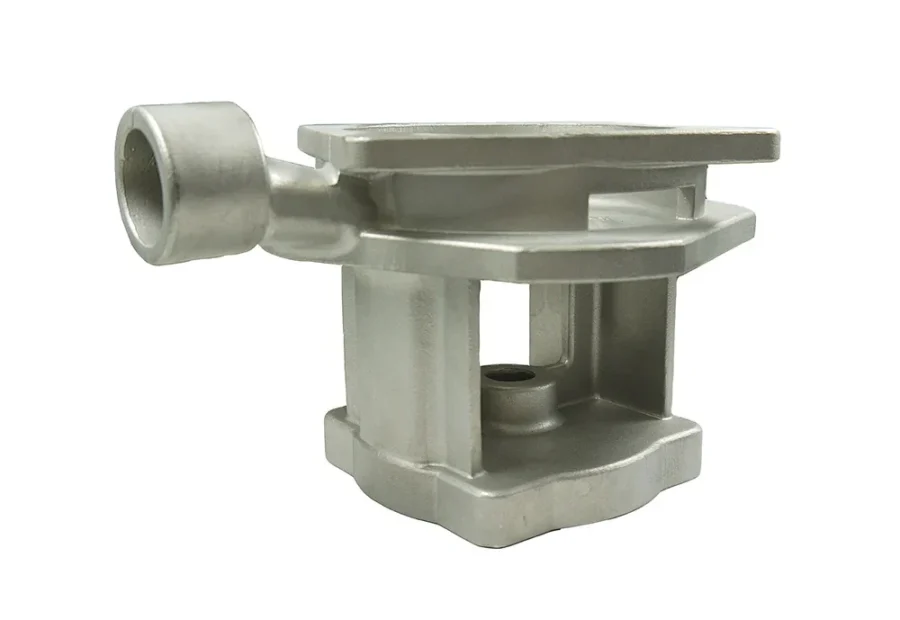
The A356 housing is the main body of an engine cooling water pump. It accommodates the impeller and water seal and forms the coolant passage. Integrated inlet and outlet connections, reinforcing ribs and several threaded mounting bosses make the geometry more involved than a simple cover casting. The supplied project record describes a 3.5–8 mm principal wall range and T6 treatment after low-pressure casting.
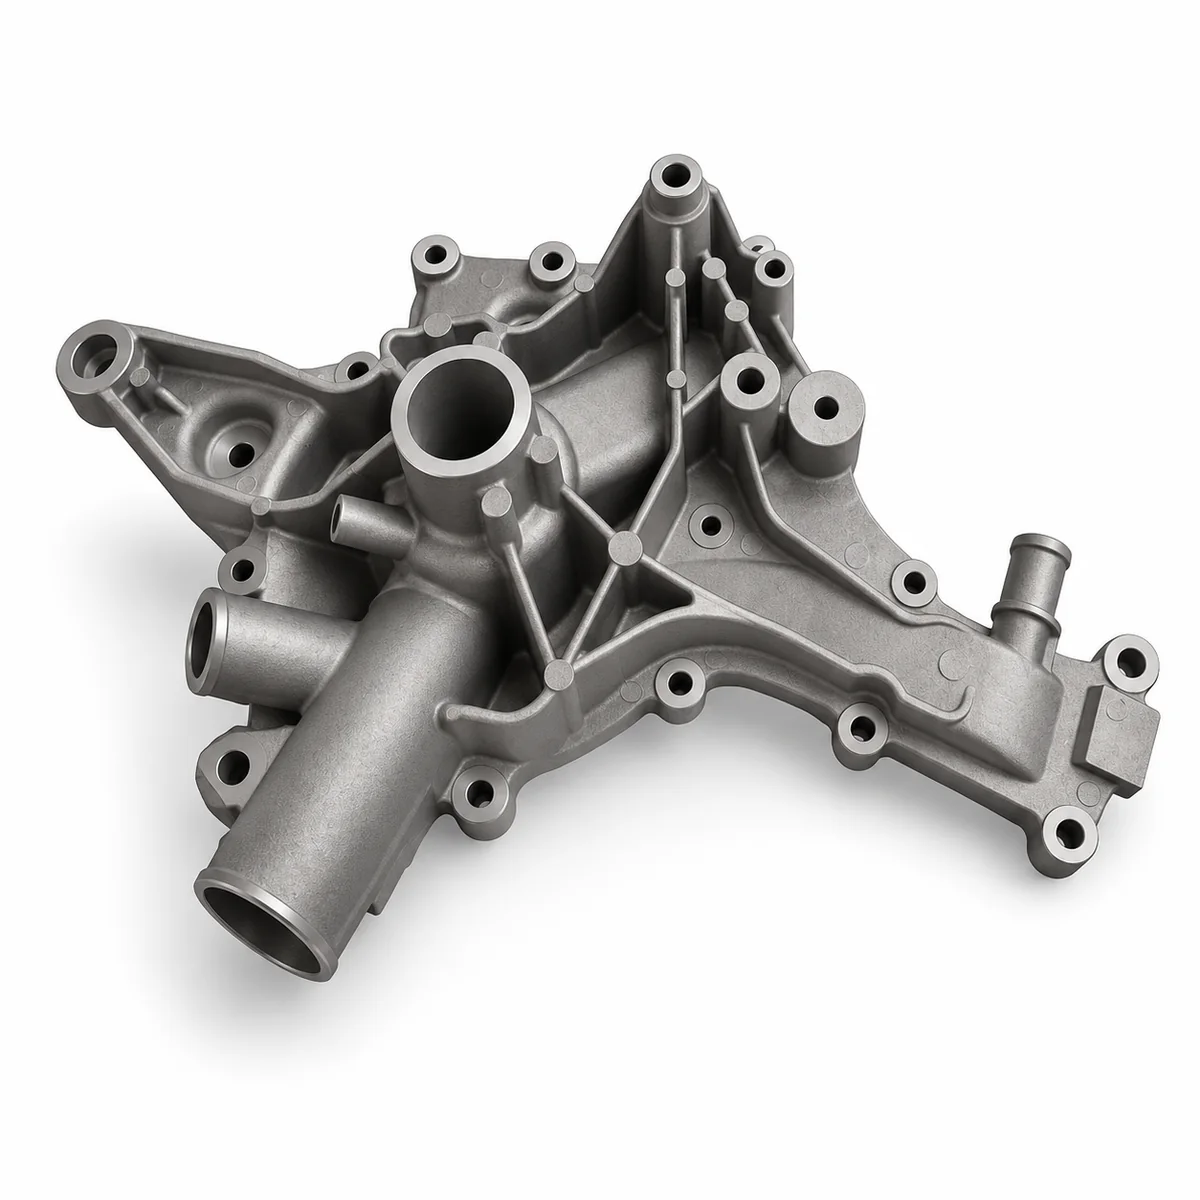
Customer requirements
The customer needed a sound casting around the pressure boundary and a defect-free sealing face. The bearing seat, flange face, pipe connection faces and bolt locations had to remain suitable for CNC finishing and assembly. The project specified an IT7 bearing bore and 0.03 mm flatness at the sealing face after machining.
Problem encountered
During production development, the thicker mounting bosses showed a tendency to shrinkage porosity. This was a critical area because the bosses connect to thin walls and sit near machined interfaces. The tight position requirements for several holes and the risk of thin-wall movement also complicated machining planning.
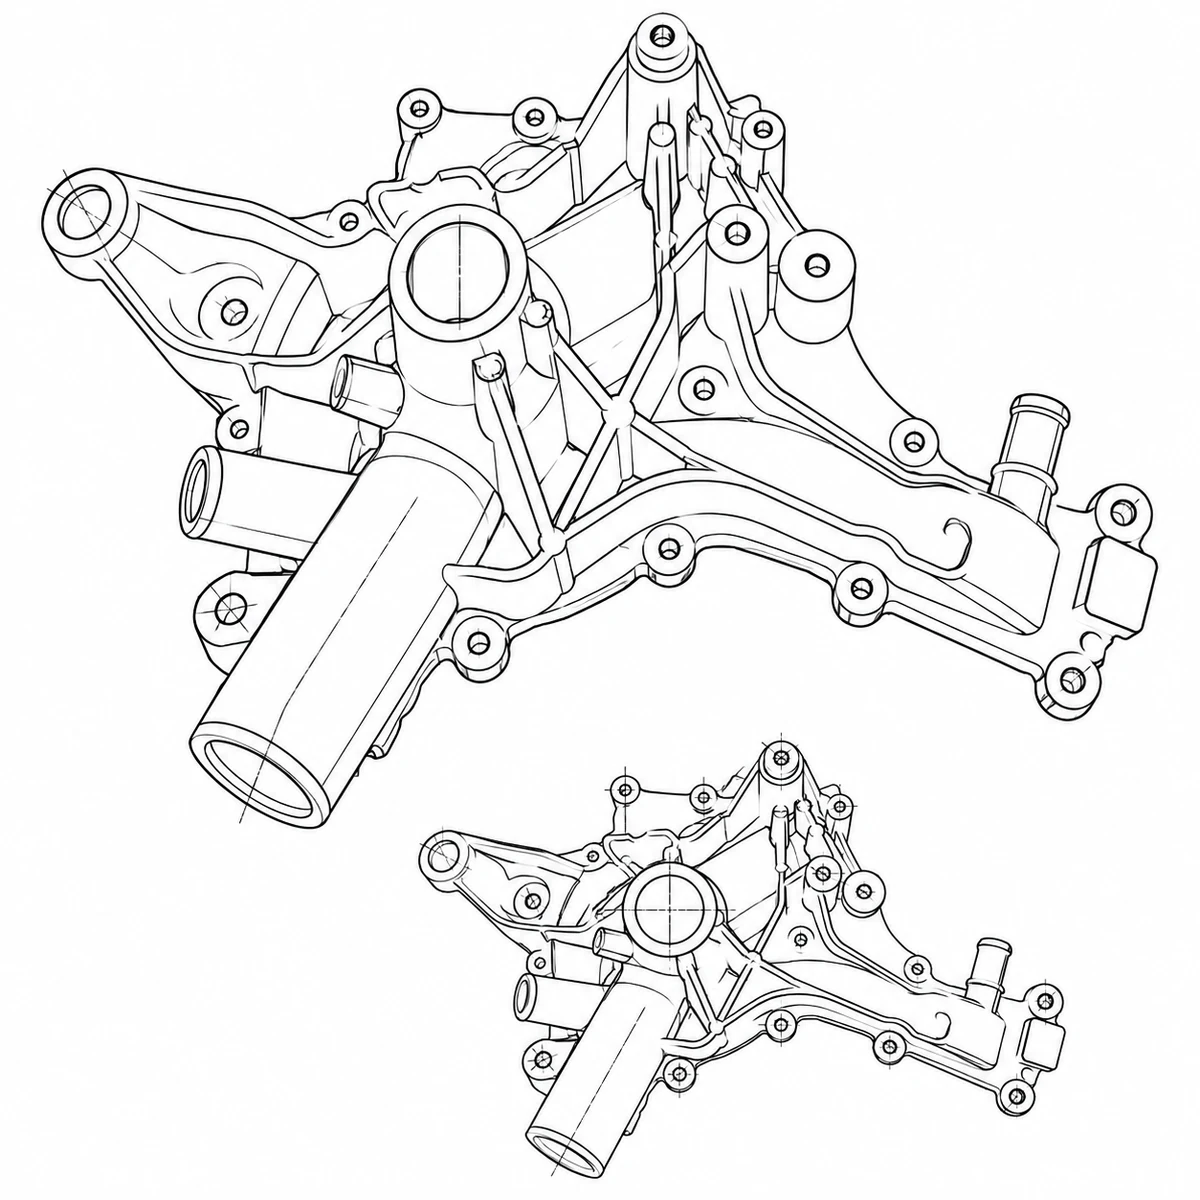
Process changes
The project used a dedicated low-pressure casting mold. The feeding arrangement around the bosses and the cooling sequence were revised to address the local shrinkage risk. After casting, the parts received T6 treatment, surface blasting and deburring before the specified CNC operations.
Machining and inspection
CNC work covered the flange mounting face, bearing-seat bore, inlet and outlet faces and bolt holes. Inspection combined furnace material analysis, CMM dimensional checks, visual examination and hydrostatic leak testing. The supplied test result records no leakage at 0.3 MPa after a 3-minute hold.
Reported project result
The project record reports that the boss-area defect was brought under control and the defect rate was held within 0.8% during batch supply. That figure is specific to this project.